
English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

Industry News
We are happy to share relevant industry news with you, as well as some developments in the industry, industry knowledge and more.
Starting a Water ATM Business in 2026: The Ultimate Guide to Equipment, Cost, and Social Impact
How to start a Water ATM Machine business in 2026: Water ATM Machine Price, RO filtration, solar power, and the Uganda Drinking Water Station project that delivered clean water in two days.
The Future of Water Vending: How IoT-Enabled "Smart Water Chambers" Drive 40% Higher ROI
Learn how IoT-enabled Smart Water Chambers transform water vending into a high-ROI asset with remote monitoring and predictive maintenance, cutting maintenance visits by 50% while ensuring 99.9% uptime for commercial drinking water services.
How to Start a Profitable Water Refilling Business: 2026 Guide to Modular Water Vending Machines
Starting a successful water refilling business in 2026 requires moving beyond traditional setups to modular Water Vending Machines (Water Kiosks). By integrating RO filtration, intelligent interaction, and modular housing into a single Water Space Station, operators can reduce site construction costs by 60% and achieve faster ROI through flexible, unmanned operations.
 14 2026-09
How Does the 304 Stainless Steel Water Supply Purifier Machine Deliver Zero‑Waste Safe Drinking Water for Rural Homes?
VLLRO's 304 Stainless Steel Water Supply Purifier Machine (Model 1000L/H) is an all‑in‑one water supply and purification solution designed for rural homes using well water or groundwater. Combining a kitchen sink, pressure tank, ultrafiltration membrane, and UV sterilizer in one compact unit, it produces zero wastewater while preserving healthy minerals. The 304 food‑grade stainless steel tank offers a lifespan of 20+ years, and the washable ultrafiltration membrane ensures low maintenance. With UV sterilization achieving a 99.9% kill rate, this system delivers safe, clean drinking water without the water waste of traditional RO systems. Backed by VLLRO's 15+ years of water treatment expertise, it is ideal for areas with limited water resources.
 04 2026-09
How Does a Containerized RO Plant Deliver Turnkey Pure Water Anywhere in the World?
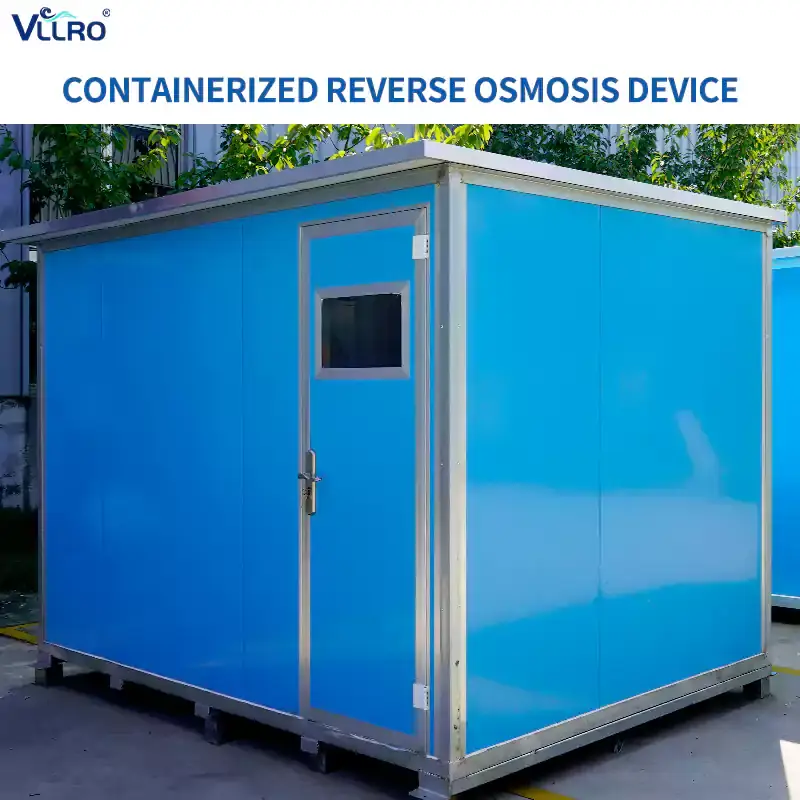
VLLRO's Containerized RO Plant is a fully integrated, factory‑assembled water purification system housed in a standard ISO container. Designed for rapid deployment, it requires only water inlet, power, and product water connections to start producing pure water—ideal for remote areas, emergency relief, industrial sites, and communities with underdeveloped infrastructure. With pretreatment, reverse osmosis, and advanced controls built in, it offers customized solutions for diverse feed water qualities. Backed by VLLRO's 15+ years of experience, two modern factories (12,000 m²), and a 72‑hour extreme pressure test for every unit, this system delivers reliable, high‑purity water across 50+ countries, from the Qinghai‑Tibet Plateau to the Middle East.
 01 2026-09
How Does a Reverse Osmosis Water Treatment System Deliver Consistent Pure Water for Commercial and Industrial Applications?
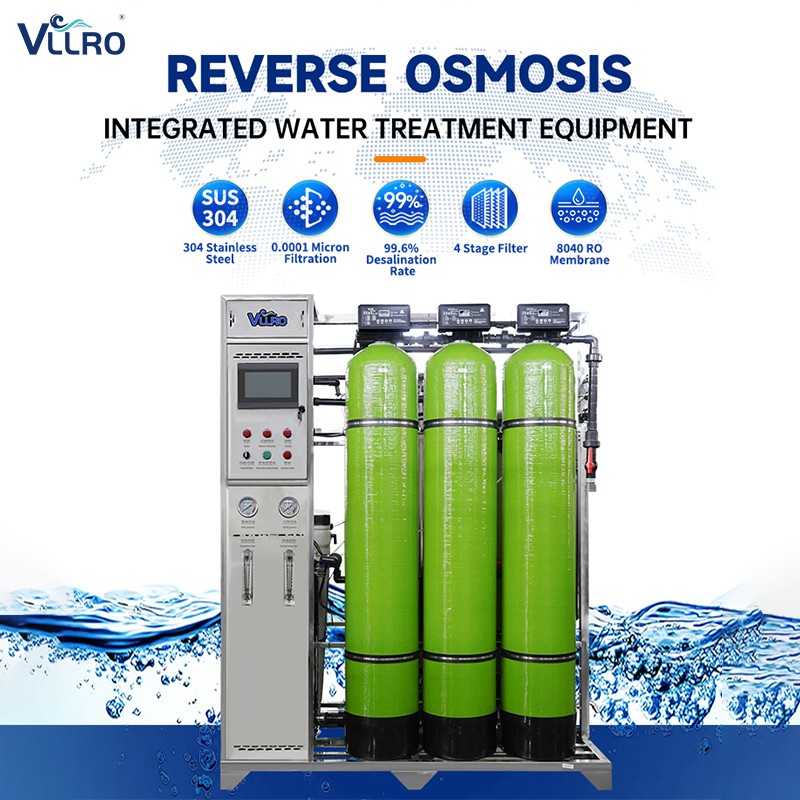
Access to reliable, high‑purity water is essential for many industries, from food processing to electronics manufacturing. The Reverse Osmosis Water Treatment system from VLLRO offers a complete, customisable solution that combines multi‑stage pre‑treatment, advanced RO membrane technology, and intelligent controls. With a production capacity ranging from 150 to 100,000 litres per hour and a desalination rate of 99.4%, this system delivers consistent water quality that meets or exceeds international standards. This article explores its technical configuration, key advantages, application versatility, and the manufacturing expertise that positions VLLRO as a trusted global supplier.