
English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

Industry News
We are happy to share relevant industry news with you, as well as some developments in the industry, industry knowledge and more.
 24 2026-08
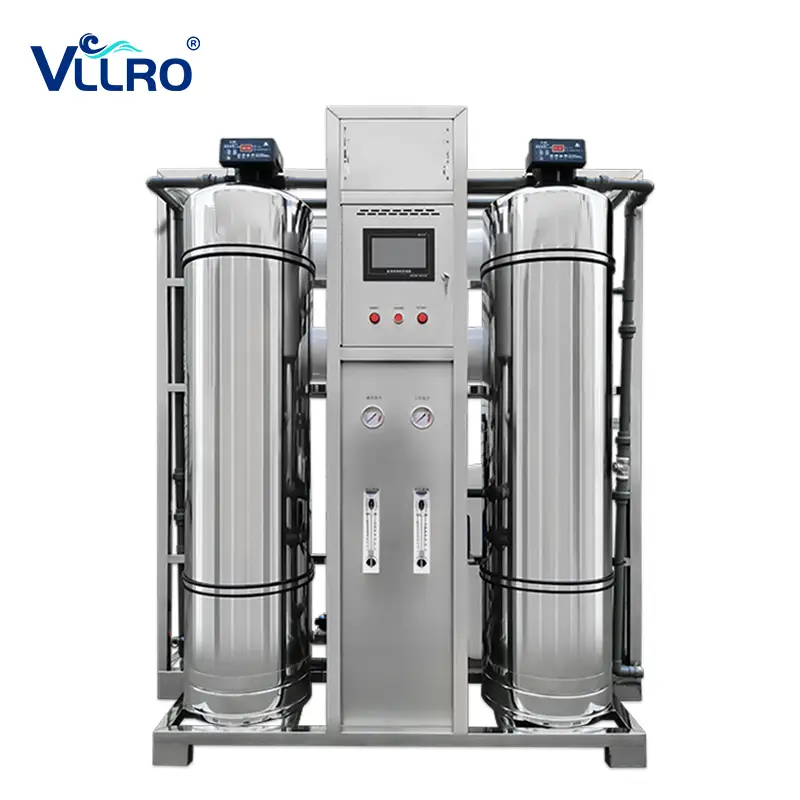
How Does an Industrial Reverse Osmosis Water Purifier Deliver Reliable High‑Purity Water for Manufacturing and Processing?
Industrial production often demands large volumes of consistent, high‑purity water for cleaning, processing, or product formulation. The Industrial Reverse Osmosis Water Purifier from VLLRO offers a robust, customisable solution that combines multi‑stage pre‑treatment, high‑efficiency RO membranes, and intelligent controls to produce up to 100 tons of pure water per hour. With a desalination rate of 99.4‑99.6%, this equipment supports applications ranging from food and beverage processing to electronics manufacturing. This article examines its technical configuration, key advantages, and the manufacturing expertise behind the VLLRO brand.
 20 2026-08
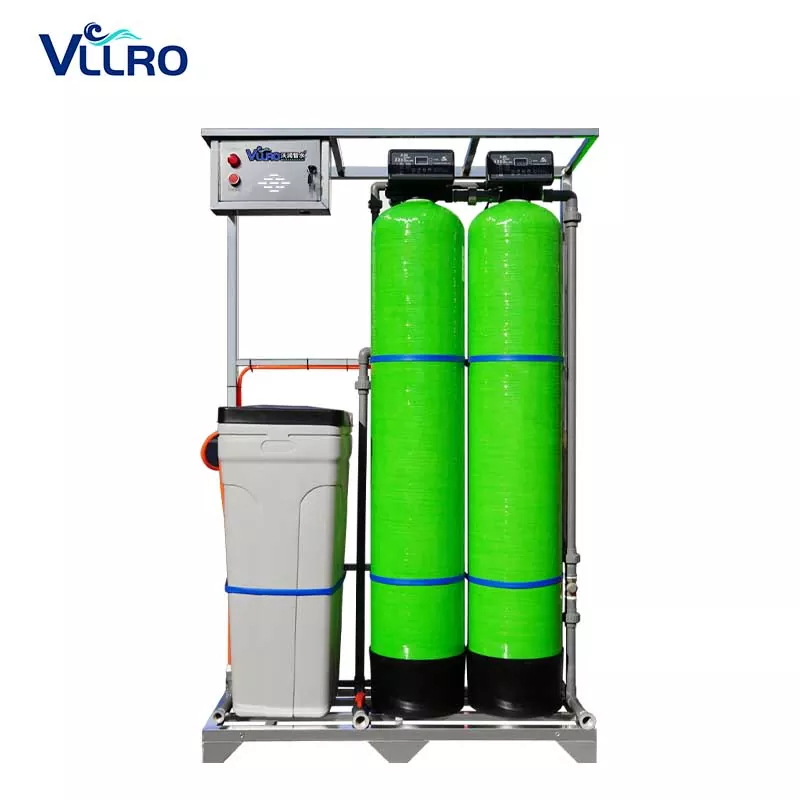
Why Is a Softening Water Filter the Smart Choice for Scale‑Free Water and Extended Appliance Life?
Hard water is a common problem worldwide, causing scale buildup in pipes, reducing the efficiency of water heaters, and leaving spots on fixtures. The Softening Water Filter from VLLRO uses advanced ion‑exchange resin technology to remove calcium and magnesium ions, delivering soft water that protects equipment, saves energy, and improves daily comfort. Available in single‑, double‑, and three‑bottle configurations, these automatic systems offer stable performance, low operating costs, and easy regeneration. This article explores the technology, product options, and application scenarios that make VLLRO a trusted name in water treatment.
 17 2026-08
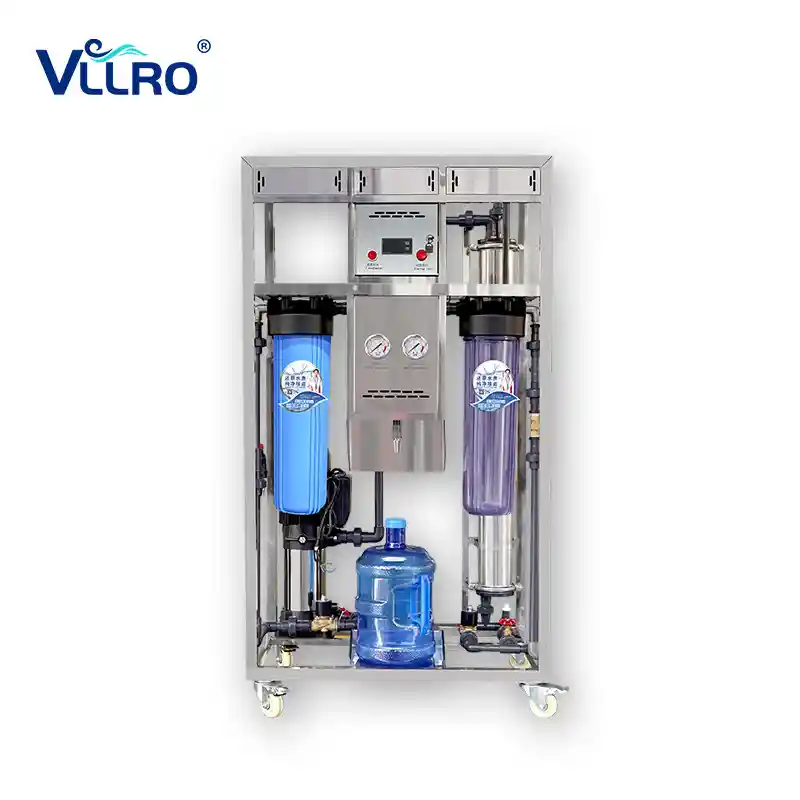
How Does a Reverse Osmosis Water-Making Machine Deliver Safe, Pure Drinking Water for Communities and Businesses?
Access to clean drinking water is a growing global concern – from urban communities to remote construction sites. The Reverse Osmosis Water-Making Machine from VLLRO offers a compact, efficient solution that removes impurities, bacteria, and viruses through a multi‑stage filtration process. With a production capacity of 0.15 tons per hour and a desalination rate of 99.4%, this equipment is designed for commercial, institutional, and community applications. This article explores its core technology, application scenarios, and the manufacturing excellence behind the VLLRO brand.
 10 2026-08
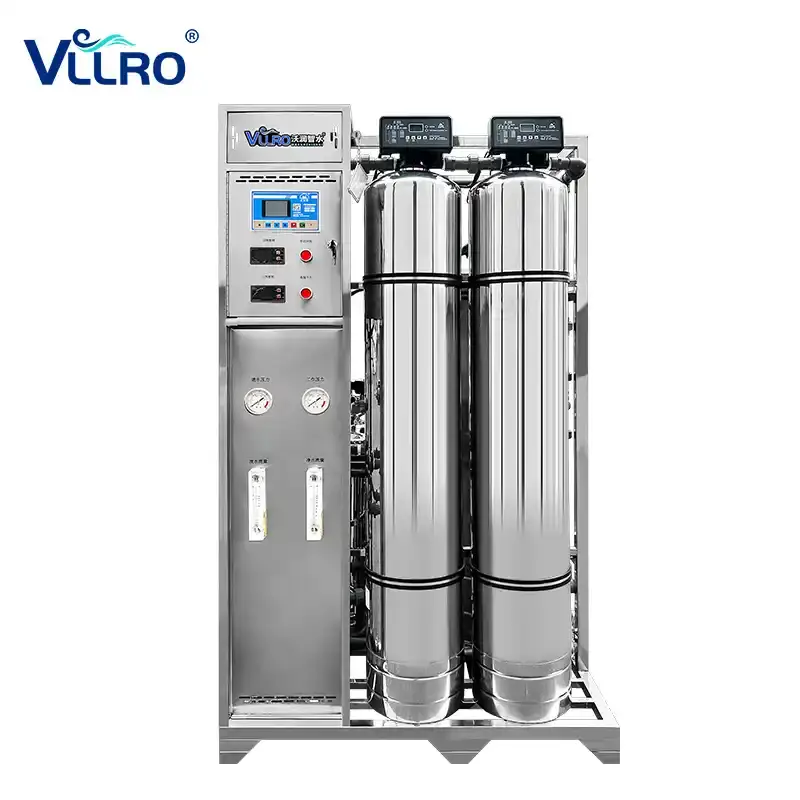
Why Is the Ultrafiltration Purification Water System a Reliable Choice for Safe and Efficient Water Treatment?
Clean water is fundamental to health, industry, and daily life. Yet many water treatment methods rely on chemical additives or complex processes that introduce secondary pollution risks or high operating costs. The Ultrafiltration Purification Water System from VLLRO offers a physical filtration solution that effectively removes suspended solids, bacteria, and viruses while preserving beneficial minerals. With fully automatic backwashing, modular pretreatment options, and low energy consumption, this system is designed for drinking water treatment, industrial applications, and municipal water supply. This article examines the product's specifications, key advantages, and the practical benefits that make it a versatile choice for diverse water treatment needs.
 07 2026-08
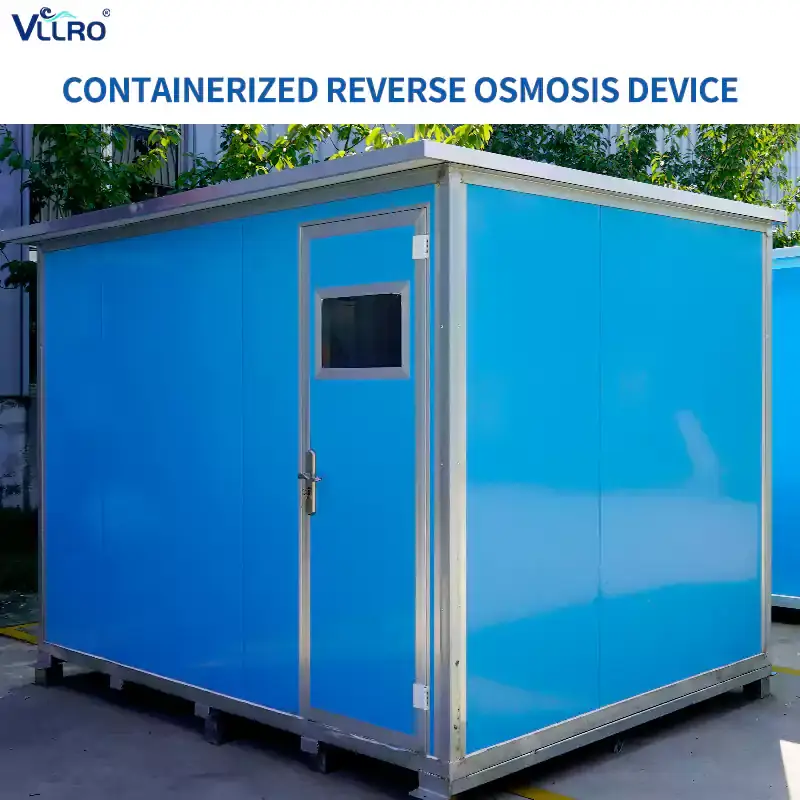
Why Is the Containerized RO Plant a Game-Changer for Rapid Deployment Water Purification in Remote and Emergency Settings?
Access to clean drinking water remains a challenge in remote areas, regions with underdeveloped infrastructure, and emergency situations where rapid response is critical. Traditional water treatment plants require extensive civil works, lengthy installation timelines, and significant on-site labor—luxuries that are often unavailable when time and resources are limited. The Containerized RO Plant from VLLRO offers a practical alternative. All water treatment components—including pretreatment, reverse osmosis, and control systems—are pre-installed inside standard ISO shipping containers at the factory. This approach eliminates the need for complex on-site assembly, reduces construction time, and enables rapid deployment to virtually any location. This article examines the product's features, applications, and the manufacturing quality that makes it a reliable solution for communities, industries, and emergency responders worldwide.
 03 2026-08
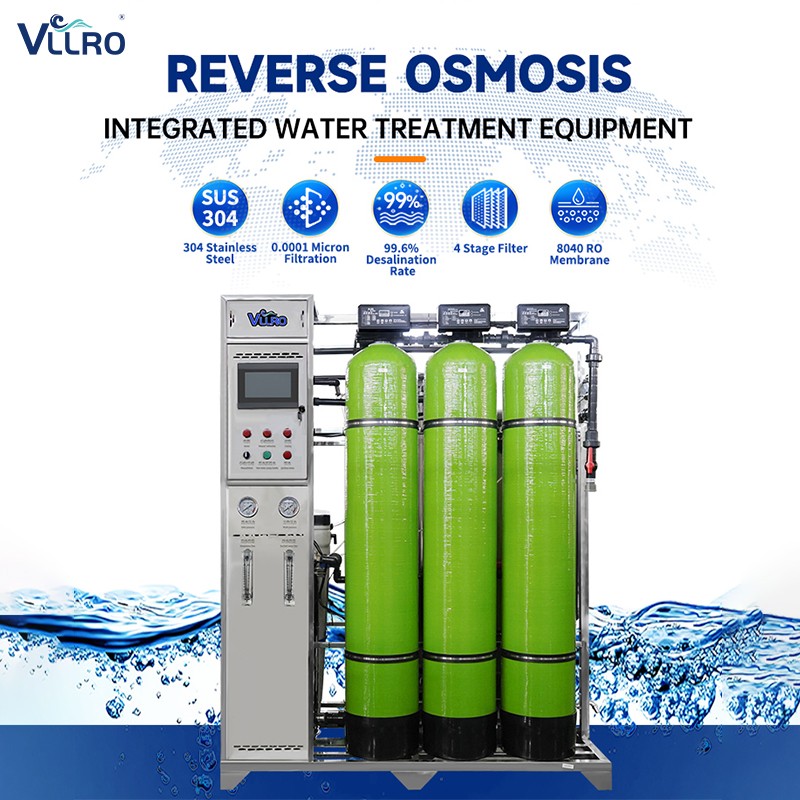
Why Is Reverse Osmosis Water Treatment the Ideal Solution for High-Purity Water Needs Across Industries?
From food and beverage production to electronics manufacturing and commercial facilities, the demand for consistently pure water continues to grow. The Reverse Osmosis Water Treatment system from VLLRO offers a reliable, efficient solution for producing high-purity water with a desalination rate of 99.40%. Featuring a multi-stage pre-treatment system, advanced RO membranes, and an intelligent control system, this equipment delivers stable water production while minimizing waste and energy consumption. This article examines the product's specifications, key features, and the applications where it delivers significant value for both residential and commercial users.