English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

How Does a Containerized RO Plant Deliver Turnkey Pure Water Anywhere in the World?
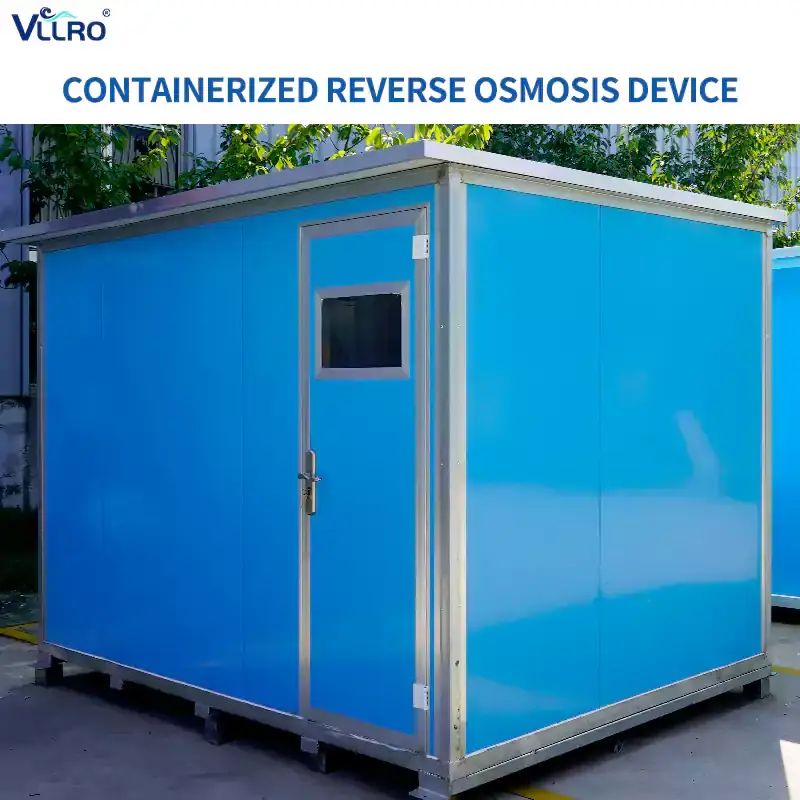
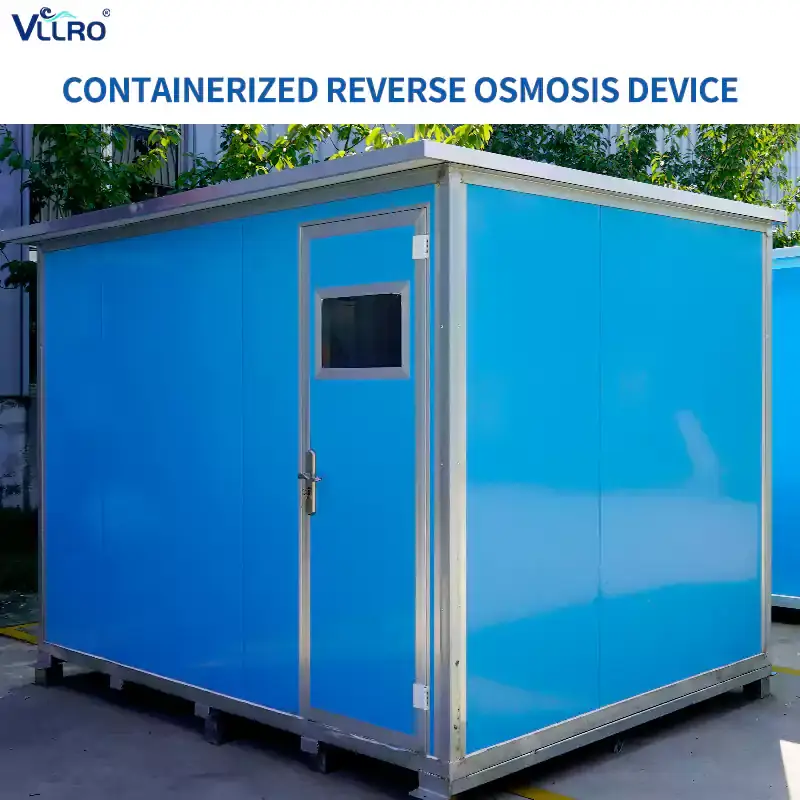
VLLRO's Containerized RO Plant is a fully integrated, factory‑assembled water purification system housed in a standard ISO container. Designed for rapid deployment, it requires only water inlet, power, and product water connections to start producing pure water—ideal for remote areas, emergency relief, industrial sites, and communities with underdeveloped infrastructure. With pretreatment, reverse osmosis, and advanced controls built in, it offers customized solutions for diverse feed water qualities. Backed by VLLRO's 15+ years of experience, two modern factories (12,000 m²), and a 72‑hour extreme pressure test for every unit, this system delivers reliable, high‑purity water across 50+ countries, from the Qinghai‑Tibet Plateau to the Middle East.

Plug‑and‑Play Pure Water for Any Environment
Traditional water treatment plants require extensive civil works, long installation times, and significant on‑site engineering. VLLRO's Containerized RO Plant eliminates these challenges. All equipment— including pretreatment filters, reverse osmosis membranes, high‑pressure pumps, and control systems—is fully installed and tested within a rugged ISO standard container at our factory in Qingdao, China. Upon arrival at the destination, users simply connect the raw water inlet, power supply, and product water outlet, and the system is ready to operate. This plug‑and‑play approach dramatically shortens project timelines, reduces civil engineering costs, and minimises installation errors. Whether deployed in a desert, a mountain camp, or a disaster‑stricken area, the containerised design ensures rapid, reliable water purification without the need for specialised on‑site construction.
Key Advantages and Customisation Options
VLLRO's containerised RO plant offers several distinct benefits that set it apart from conventional systems:
• Factory Pre‑installation – All components are mounted, piped, and wired in our controlled workshop, ensuring consistent quality and eliminating field assembly errors.
• Quick Deployment – From delivery to operation in hours, not months—ideal for emergency water supply and temporary installations.
• Reduced Civil Works – No need for dedicated pump rooms, chemical storage buildings, or extensive foundations; the container serves as the equipment shelter.
• Customisable Pretreatment – Tailored to your raw water quality (e.g., high turbidity, iron, hardness, or salinity) with options for multimedia filters, activated carbon, softeners, and chemical dosing.
• Energy‑Efficient Operation – Advanced energy‑recovery devices and variable‑frequency drives lower power consumption and operating costs.
• Remote Monitoring – Optional IoT connectivity enables real‑time performance tracking and alarm notifications from anywhere.
Technical Specifications
| Parameter | Specification |
| Container Type | 20‑ft or 40‑ft ISO standard (customisable) |
| Production Capacity | 0.5 – 100 m³/h (customisable) |
| Feed Water Source | Municipal, brackish, seawater (with appropriate pretreatment) |
| Product Water Quality | ≤ 10 μS/cm (drinking water or industrial grade, customisable) |
| Recovery Rate | 60% – 75% (brackish); 35% – 50% (seawater) |
| Power Supply | 380V/50Hz or 460V/60Hz (customisable) |
| Control System | PLC with HMI, auto‑start/stop, fault alarms, data logging |
| Heating/Insulation | Optional for sub‑zero environments (as in Qinghai‑Tibet case) |
| Warranty | 1 year (whole system), extended options available |
Application Scenarios
VLLRO's containerised RO plant has been deployed in diverse settings across the globe:
• Remote Communities and Off‑Grid Areas – Provides safe drinking water where no pipeline infrastructure exists; used in African villages, island resorts, and mountain settlements.
• Industrial and Mining Sites – Supplies process water for manufacturing, mining operations, and oil/gas exploration, reducing reliance on trucked‑in water.
• Emergency Relief and Disaster Response – Deployed after earthquakes, floods, or hurricanes to restore clean water quickly; compact and air‑freightable.
• Military and Humanitarian Missions – Supports field operations with self‑contained, low‑maintenance water production.
• High‑Altitude and Extreme Climates – Customised with heating and insulation for the Qinghai‑Tibet Plateau, where temperatures drop below -30°C, ensuring year‑round operation.
VLLRO – Manufacturing Excellence and Global Reach
Jianyun Zhishui (Qingdao) Industrial Technology Co., Ltd. (brand VLLRO) has over 15 years of experience in water treatment. Headquartered in Qingdao, a world‑class port city, the company operates two modern production bases totalling 12,000 m², with highly automated assembly lines and an annual capacity of over 20,000 units. Every containerised RO plant undergoes a rigorous 72‑hour extreme pressure simulation test before shipping, verifying sealing, structural integrity, and operational stability. The factory is equipped with laser cutting machines, CNC machining centres, and robotic welding systems, ensuring millimeter‑level precision. VLLRO holds ISO 9001, CE, and other certifications, and has served customers in more than 50 countries, including Southeast Asia, the Middle East, Europe, the Americas, and Africa. The company's engineering team provides free custom design based on your raw water quality and flow requirements, ensuring optimal system performance.
Service and Support
VLLRO offers a comprehensive service package to ensure long‑term satisfaction:
• Pre‑Sales – Free water analysis, system design, and capacity recommendation.
• In‑Sales – Detailed production tracking, factory acceptance testing, and quality documentation.
• After‑Sales – Installation manuals, video guides, remote online support, and lifelong spare parts supply. A dedicated team of engineers is available via phone, email, and remote connection to troubleshoot issues promptly.
VLLRO also provides OEM/ODM services, including custom colours, branding, control logic, and component selection to meet specific market requirements. With a strong logistics network, shipments can be delivered to any port worldwide efficiently.
Frequently Asked Questions
Q: What is the typical delivery time for a containerised RO plant?
A: For standard configurations, delivery is 30‑45 days. Customised orders may take 45‑60 days depending on complexity and component availability.
Q: Can the system treat seawater?
A: Yes. With high‑pressure pumps and seawater RO membranes, we can design a system for seawater desalination with recovery rates of 35‑50%.
Q: What pretreatment is required?
A: This depends on feed water quality. We offer multimedia filters, carbon filters, softeners, and chemical dosing to protect the RO membranes and ensure long‑term operation.
Q: Is the equipment suitable for freezing temperatures?
A: Yes. We provide heating and insulation packages for sub‑zero environments, as successfully deployed on the Qinghai‑Tibet Plateau.
Q: Do you offer rental or leasing options?
A: Yes, for short‑term projects or emergency response, we can discuss rental arrangements. Please contact our sales team for details.
Q: Can I visit the factory before ordering?
A: Absolutely. We welcome visitors to our Qingdao facility to inspect production processes and witness factory testing firsthand.
Conclusion
In summary, VLLRO's Containerized RO Plant offers a fast‑deploy, cost‑effective, and highly reliable solution for pure water production in any location—from remote villages to industrial complexes. With factory pre‑installation, customisable configurations, and a proven track record across 50+ countries, it eliminates the hassles of traditional plant construction. For technical discussions, custom design, or a prompt quotation, please reach out to our team today—we are ready to engineer the right water solution for your needs.
Related News
- How to Reduce Wastewater in Commercial RO Systems Without Sacrificing Membrane Life
- How to Calculate ROI for a Commercial Water Refilling Station
- How to Design a Borehole Water Pretreatment System for Remote Commercial RO Stations
- The "Brain" Behind the System: How VLLRO's Intelligent IoT Control Platform Revolutionizes Water Management
- The Invisible Shield: Why UV Sterilization is Non-Negotiable for Safe Drinking Water
- Maximizing RO Longevity: The Complete Guide to Water Filtration Consumables and Replacement Cycles
Leave me a message