English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

How Does a Reverse Osmosis Water Treatment System Deliver Consistent Pure Water for Commercial and Industrial Applications?
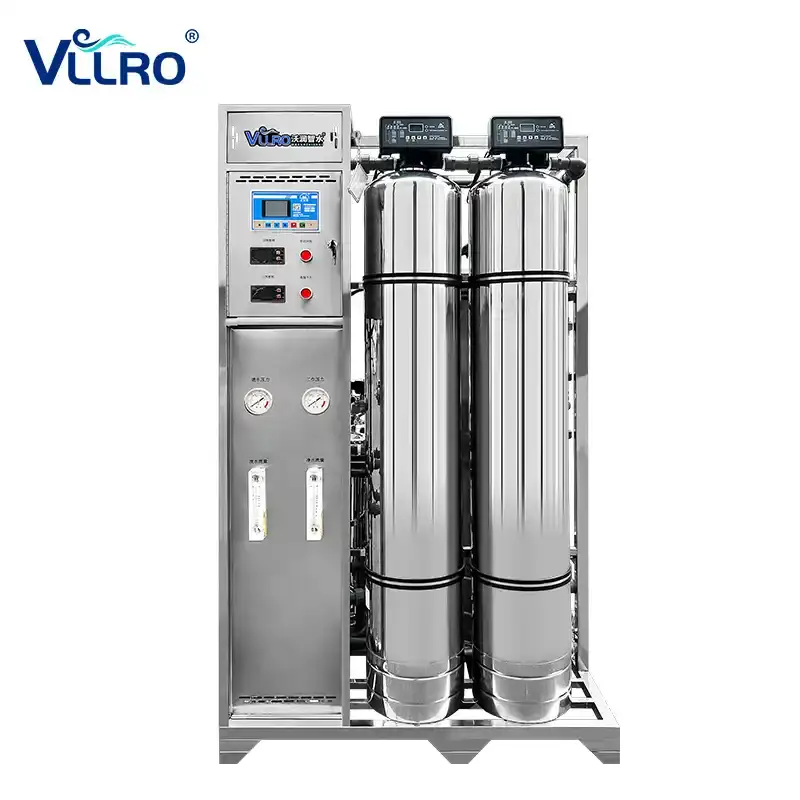
Access to reliable, high‑purity water is essential for many industries, from food processing to electronics manufacturing. The Reverse Osmosis Water Treatment system from VLLRO offers a complete, customisable solution that combines multi‑stage pre‑treatment, advanced RO membrane technology, and intelligent controls. With a production capacity ranging from 150 to 100,000 litres per hour and a desalination rate of 99.4%, this system delivers consistent water quality that meets or exceeds international standards. This article explores its technical configuration, key advantages, application versatility, and the manufacturing expertise that positions VLLRO as a trusted global supplier.

Why Reverse Osmosis Is the Gold Standard for Water Purification?
Reverse osmosis is widely regarded as the most effective water purification technology available today. By forcing water through a semi‑permeable membrane under pressure, RO systems remove up to 99.6% of dissolved salts, organic compounds, bacteria, and other contaminants. This makes it the preferred choice for industries that require consistent, high‑quality water for production, cleaning, or formulation.
The Reverse Osmosis Water Treatment system from VLLRO is designed to meet these demanding requirements. Whether you need 1 ton or 100 tons of pure water per hour, the system can be configured to match your specific flow and quality needs. With a robust pre‑treatment train and high‑performance RO membranes, it delivers reliable performance even with challenging feed water conditions.
System Configuration and Multi‑Stage Pre‑Treatment
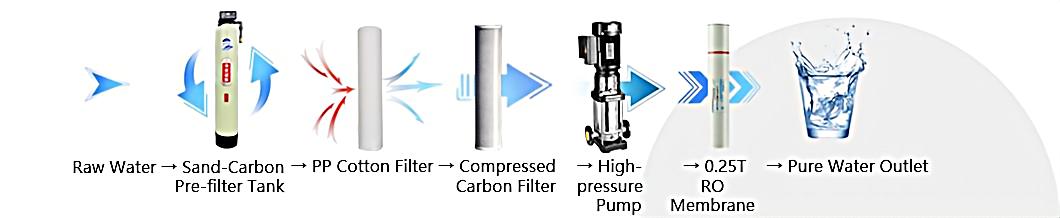
The VLLRO Reverse Osmosis Water Treatment system is built around a comprehensive pre‑treatment process that protects the RO membranes and ensures optimal performance. A typical configuration includes:
• Multi‑media filter (sand filter) – Removes suspended solids, silt, and turbidity to prevent membrane fouling.
• Activated carbon filter – Adsorbs chlorine, organic compounds, and odours that can damage RO membranes.
• Water softener (resin filter) – Reduces hardness to prevent scale formation on membrane surfaces.
• Precision security filter – Provides final particulate removal with 5‑micron PP cotton cartridges.
• Reverse osmosis membrane stage – The core purification step, using HuiTong 4040 membranes (or equivalent) to achieve high salt rejection.
This layered approach ensures that the RO membranes operate under optimal conditions, extending their lifespan and reducing maintenance frequency.
Product Specifications
The table below summarises the key parameters for the Reverse Osmosis Water Treatment system model VLLRO‑RO‑1.0 from VLLRO. Other capacities are available upon request.
| Parameter | Specification |
| Model | VLLRO‑RO‑1.0 |
| Process Flow | Sand → Carbon → Resin → Precision filter → RO membrane |
| Dimensions (L×W×H) | 101 cm × 100 cm × 162 cm |
| Water Production | 1.0 ton per hour (customisable from 150 to 100,000 L/H) |
| Desalination Rate | 99.4% |
| Voltage | 110V / 220V / 380V (selectable) |
| Inlet Pressure | 0.2 – 0.4 MPa |
| RO Operating Pressure | 0.8 – 1.2 MPa |
| RO Membrane | HuiTong 4040 × 4 (or equivalent brand) |
| High‑Pressure Pump | SHIMGE (or equivalent international brand) |
| Filter Tank | 300 × 1400 mm |
| Precision Filter | PP cotton × 5 |
| Filter Media Volume | Sand: 80 kg; Carbon: 28 kg (with 13 kg sand underbed) |
| Storage Tank | 300 L, 304 stainless steel |
| Inlet / Waste Outlet | 6' (3/4 inch) |
| Pure Water Outlet | 4' (1/2 inch) |
| Raw Water TDS Limit | <1500 ppm |
| Raw Water Temperature | 25°C (nominal) |
| Raw Water Turbidity | <5 FTU |
| Raw Water Iron Ion | <0.3 mg/L |
Intelligent Control and User‑Friendly Operation
Modern water treatment equipment must be easy to operate and maintain. The VLLRO Reverse Osmosis Water Treatment system features an intelligent control system that simplifies daily management:
• Automatic flushing – Periodically cleans the RO membranes to prevent fouling and maintain performance.
• Water shortage protection – Automatically shuts down the system when feed water pressure drops, preventing pump damage.
• Fault alarm – Alerts operators to issues such as high pressure, low flow, or membrane degradation.
• Customisable controls – The control logic can be tailored to specific requirements, including remote monitoring and integration with building management systems.
These features reduce the need for constant supervision, allowing the system to operate reliably around the clock with minimal human intervention.
Durable Construction and Space‑Efficient Design
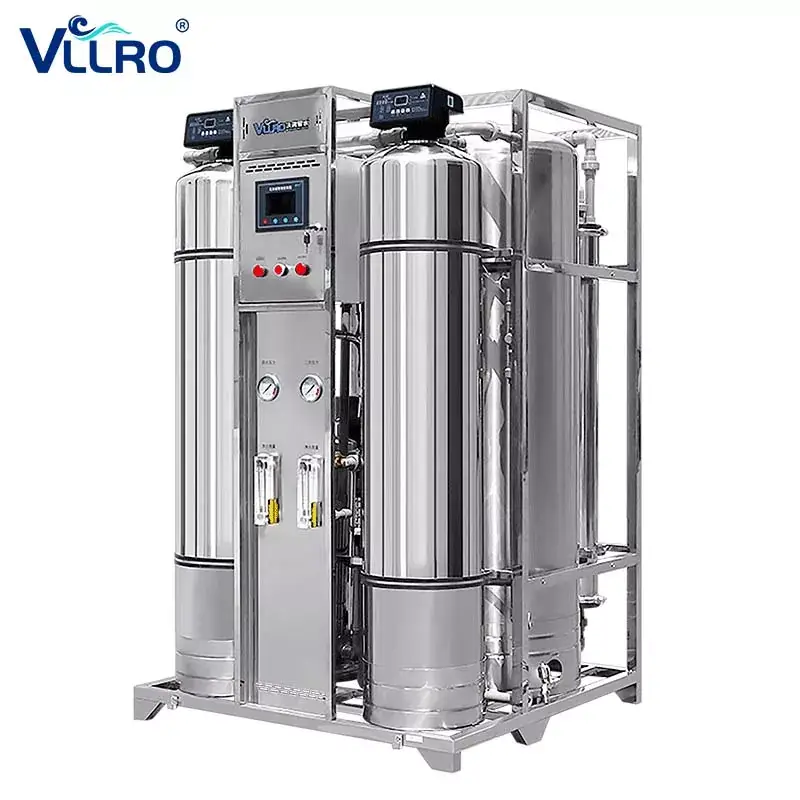
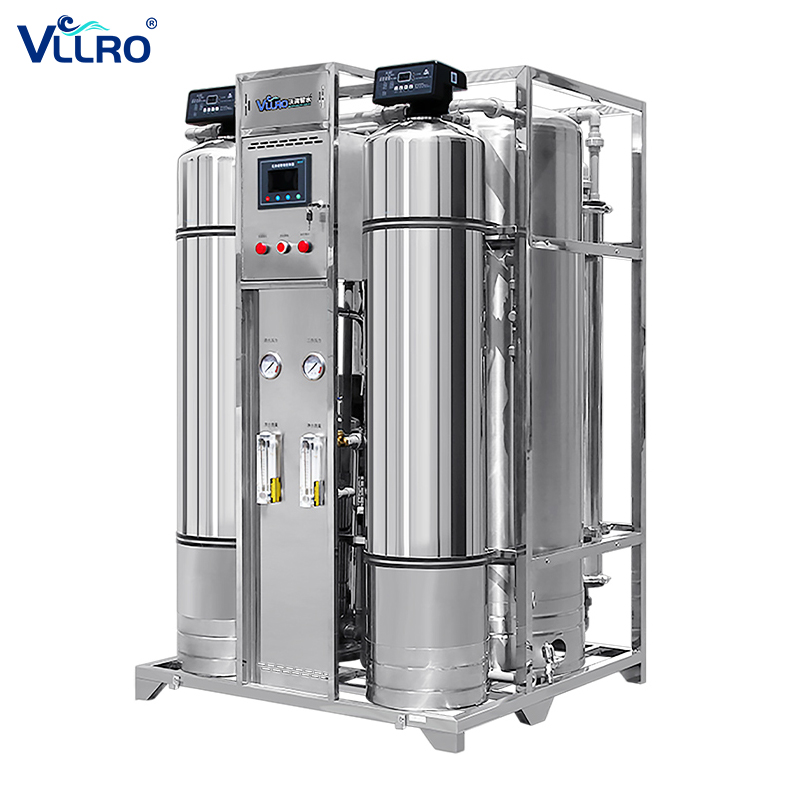
The Reverse Osmosis Water Treatment system is built with a sturdy 304 stainless steel frame that resists corrosion and rust, extending the equipment's service life. The modular layout ensures efficient use of space and provides easy access for maintenance:
• Filter media tanks – Conveniently positioned for simple media replacement.
• Pump and membrane housing – Designed with ample clearance for servicing and element changes.
• Compact footprint – The system occupies minimal floor space, making it suitable for facilities with limited room.
All components are standardised and readily available globally, simplifying spare parts procurement and reducing downtime.
Water and Energy Efficiency for Lower Operating Costs
Operating costs are a key consideration for any water treatment system. The VLLRO Reverse Osmosis Water Treatment is designed to minimise both water and energy consumption:
• Reduced wastewater discharge – The system's design optimises recovery rates, minimising the volume of concentrate water sent to drain.
• Energy‑saving technology – High‑efficiency pumps and motors reduce electricity consumption, lowering monthly utility bills.
• Low maintenance requirements – The robust pre‑treatment and high‑quality membranes reduce the frequency of cleaning and replacement.
These efficiency measures help operators achieve a lower total cost of ownership while maintaining consistent water quality.
Versatile Applications Across Multiple Industries
The Reverse Osmosis Water Treatment system is suitable for a wide range of applications:
• Food and beverage industry – Ingredient water, cleaning, and beverage preparation, ensuring product taste and safety.
• Electronics and semiconductor manufacturing – Providing ultra‑pure water for cleaning circuit boards and semiconductor components.
• Hotels and commercial centres – High‑quality water for central kitchens, swimming pools, and spa facilities.
• Schools and community water stations – Centralised drinking water supply for large groups.
• Healthcare and laboratories – Water for diagnostic equipment, sterilisation, and analytical instruments.
With customisable capacities and configurations, the system can be scaled to meet the specific needs of each application.
Manufacturing Excellence and Quality Assurance
VLLRO (Jianyun Zhishui (Qingdao) Industrial Technology Co., Ltd.) has over 15 years of experience in water treatment equipment manufacturing. The company operates two modern production bases totalling more than 12,000 square metres, equipped with advanced facilities including laser cutting machines, robotic welding systems, and automated assembly lines.
Every Reverse Osmosis Water Treatment system undergoes a rigorous 72‑hour test before dispatch, including pressure testing, performance verification, and automated program debugging. The company holds CE and ISO9001 certifications, and can also assist customers in meeting market‑specific requirements such as NSF and FDA standards. This commitment to quality and transparency has earned VLLRO the trust of over 1,000 customers in more than 50 countries worldwide.
Frequently Asked Questions
Q: What is the maximum water production capacity of this system?
A: The system can be customised to produce from 150 litres per hour up to 100,000 litres per hour, depending on the model and configuration.
Q: What is the expected desalination rate?
A: The desalination rate typically reaches 99.4%, ensuring high‑purity water suitable for most commercial and industrial applications.
Q: Can the system handle raw water with high turbidity or TDS?
A: Yes, the pre‑treatment section (sand, carbon, and softener filters) is designed to handle turbidity below 5 FTU and TDS up to 1500 ppm. For higher TDS, additional pre‑treatment or a two‑stage RO design is available.
Q: Is the system easy to install and operate?
A: Absolutely. The system is factory‑assembled and tested, requiring only connection to water, power, and drain lines. The intelligent control panel makes operation straightforward with minimal training.
Q: Does VLLRO offer OEM/ODM customisation?
A: Yes, VLLRO specialises in customised solutions. We can adjust capacity, materials, control systems, and branding to match your specific requirements.
Q: What certifications does the system hold?
A: The system and its components carry CE and ISO9001 certifications. We can also assist with NSF, FDA, and other market‑specific compliance.
Conclusion
The Reverse Osmosis Water Treatment system from VLLRO delivers reliable, high‑purity water for a wide range of commercial and industrial applications. With robust pre‑treatment, intelligent controls, and efficient operation, it offers a cost‑effective solution for businesses that require consistent water quality. Backed by over 15 years of manufacturing expertise, global export experience, and a commitment to customisation, VLLRO is well‑positioned to support your water treatment needs. Contact our team today to discuss your project – we will provide a detailed proposal and quotation tailored to your specific requirements.
Related News
- How to Reduce Wastewater in Commercial RO Systems Without Sacrificing Membrane Life
- How to Calculate ROI for a Commercial Water Refilling Station
- How to Design a Borehole Water Pretreatment System for Remote Commercial RO Stations
- The "Brain" Behind the System: How VLLRO's Intelligent IoT Control Platform Revolutionizes Water Management
- The Invisible Shield: Why UV Sterilization is Non-Negotiable for Safe Drinking Water
- Maximizing RO Longevity: The Complete Guide to Water Filtration Consumables and Replacement Cycles
Leave me a message