English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

Why Is the Containerized RO Plant a Game-Changer for Rapid Deployment Water Purification in Remote and Emergency Settings?
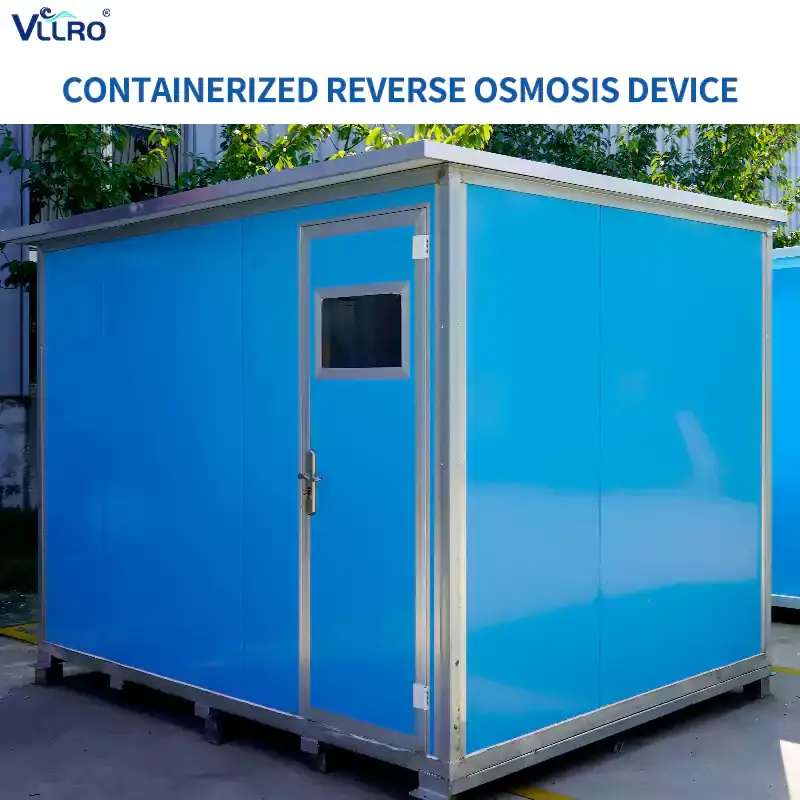
Access to clean drinking water remains a challenge in remote areas, regions with underdeveloped infrastructure, and emergency situations where rapid response is critical. Traditional water treatment plants require extensive civil works, lengthy installation timelines, and significant on-site labor—luxuries that are often unavailable when time and resources are limited. The Containerized RO Plant from VLLRO offers a practical alternative. All water treatment components—including pretreatment, reverse osmosis, and control systems—are pre-installed inside standard ISO shipping containers at the factory. This approach eliminates the need for complex on-site assembly, reduces construction time, and enables rapid deployment to virtually any location. This article examines the product's features, applications, and the manufacturing quality that makes it a reliable solution for communities, industries, and emergency responders worldwide.
The Challenge of Deploying Water Treatment in Difficult Locations
Providing clean water in remote or underserved areas is fraught with challenges. Transporting heavy equipment, sourcing skilled labor for installation, and building permanent structures can be prohibitively expensive and time-consuming. In emergency situations—such as natural disasters or humanitarian crises—the need for clean water is immediate, but traditional water treatment plants cannot be deployed quickly enough. The Containerized RO Plant from VLLRO is designed to overcome these barriers. By packaging the entire water treatment system into a standard shipping container, the solution becomes a plug-and-play unit that can be transported by truck, ship, or rail and made operational within hours of arrival.
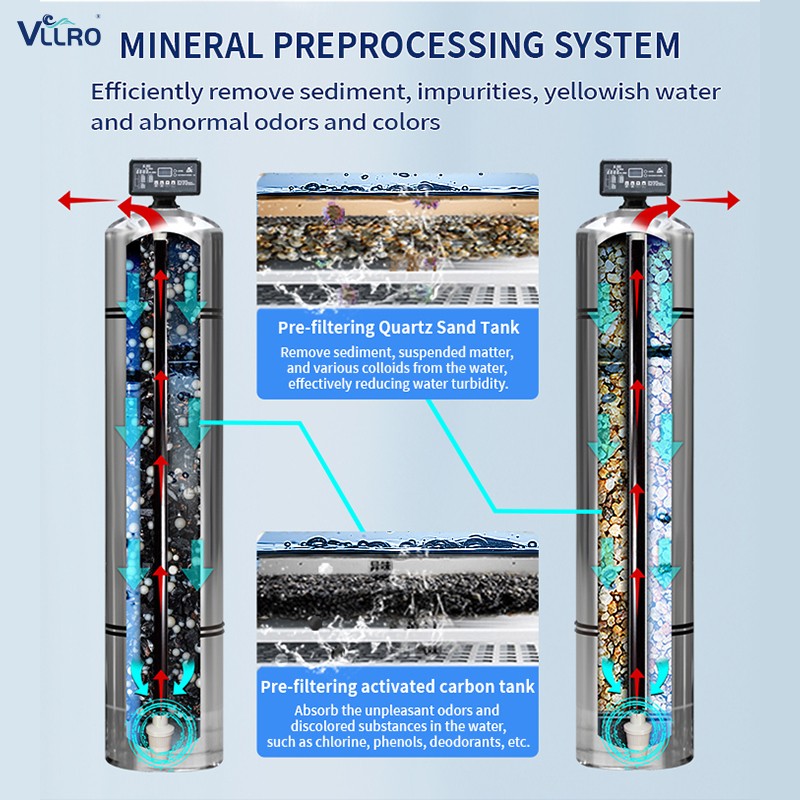
The system is built around reverse osmosis technology, which removes up to 99% of dissolved solids, bacteria, and other impurities from water. The containerized design integrates all necessary components—including multi-media filters, activated carbon filters, high-pressure pumps, RO membranes, and an intelligent control system—into a single, self-contained unit. Users only need to connect the water inlet, power supply, and product water discharge pipes to begin producing clean water. This simplicity makes the system accessible to operators with varying levels of technical expertise, further reducing the barriers to deployment.
Key Features and Advantages
The product offers several features that make it a practical choice for rapid deployment and long-term operation in challenging environments.
| Feature | Description | Benefit |
| Factory Pre-Installation | All components installed inside ISO container at the factory | Eliminates on-site assembly, reduces installation time and errors |
| Plug-and-Play Operation | Connect inlet, power, and outlet—ready to operate | Rapid deployment, minimal training required |
| Customizable Pretreatment | Tailored pretreatment systems based on raw water quality | Ensures long-term stable operation and RO membrane protection |
| Robust Construction | Built to withstand harsh environments and transportation | Durable, low maintenance, suitable for extreme conditions |
| Cold Weather Adaptability | Custom heating and insulation systems for extreme climates | Enables operation in sub-zero temperatures |
| Intelligent Control System | Automated monitoring and operation | Simplifies operation, reduces manpower requirements |
These features combine to make the system a practical solution for a wide range of applications, from community water supply in remote regions to emergency response and industrial use.
Applications Across Diverse Settings
The Containerized RO Plant is suitable for a variety of applications:
• Remote communities – Provides a reliable source of clean drinking water for villages and towns without access to municipal water supplies, significantly improving public health and quality of life.
• Emergency response – Deployed rapidly after natural disasters to provide safe water for displaced populations, supporting humanitarian aid efforts and reducing the risk of waterborne diseases.
• Industrial operations – Supplies pure water for remote mining sites, oil and gas operations, and construction projects, ensuring compliance with environmental and operational requirements.
• Military and defense – Provides self-contained water purification for forward operating bases and field operations, reducing logistical dependence on bottled water.
• Infrastructure development – Supports temporary worker camps and infrastructure projects in areas where permanent water treatment is not yet available.
• Tourism and hospitality – Supplies clean water for resorts and hotels in remote locations, enhancing guest experience and operational sustainability.
The versatility of the containerized design allows the system to be adapted to different water sources and quality requirements, making it a flexible solution for diverse scenarios.
Real-World Application: Pure Water on the Qinghai-Xizang Plateau
A compelling example of the product's capabilities is its deployment on the Qinghai-Xizang Plateau, one of the highest and most challenging environments on Earth. Local schools, communities, and hospitals require a stable supply of pure water, but the region's extreme cold—with temperatures dropping to minus tens of degrees Celsius—poses significant challenges for conventional water treatment equipment. VLLRO customized the Containerized RO Plant with specialized heating and insulation systems to ensure stable operation in these harsh conditions. The result: a reliable source of clean drinking water for local residents, even during the coldest months of the year.
This case demonstrates the system's adaptability to extreme environments and its ability to meet the specific needs of diverse users. The factory-pre-installed design and customizable pretreatment options ensure that the system can be tailored to local conditions, whether the challenge is low temperatures, high salinity, or other water quality issues. The project highlights the practical value of containerized water treatment solutions in regions where traditional approaches are not feasible.
Quality Assurance and Manufacturing Capabilities
VLLRO is backed by Jianyun Zhishui (Qingdao) Industrial Technology Co., Ltd., a water treatment equipment manufacturer with over 15 years of industry experience. The company operates two modern production bases totaling more than 12,000 square meters, equipped with advanced facilities including laser cutting machines, welding robots, and automated assembly lines. All equipment undergoes rigorous factory testing—including pressure tests, performance tests, and automated program debugging—to ensure that it meets the required standards before shipment.
The company's location in Qingdao, one of the world's busiest ports, provides convenient access to global shipping routes, enabling fast and cost-effective delivery to customers worldwide. The engineering team provides ongoing support via phone, email, and remote connection, ensuring that customers receive assistance whenever needed. CE and ISO 9001 certifications confirm the product's compliance with international quality and safety standards.
Frequently Asked Questions
Q: How long does it take to install and commission the containerized RO plant?
A: The system is designed for rapid deployment. With all components pre-installed at the factory, on-site installation typically takes hours rather than weeks. Users simply connect the water inlet, power supply, and product water discharge pipes to begin operation.
Q: Can the system be customized for specific water quality challenges?
A: Yes, the pretreatment system can be customized based on raw water quality analysis. VLLRO's engineering team can tailor the system to address specific challenges such as high salinity, turbidity, or chemical contamination.
Q: What is the typical water production capacity of a containerized RO plant?
A: Capacity varies depending on the specific configuration. Systems can be designed to meet a wide range of production requirements, from small community supplies to larger industrial-scale operations. Contact the sales team for detailed specifications based on your needs.
Q: Does the system require skilled operators?
A: The intelligent control system simplifies operation, making it accessible to users with varying levels of technical expertise. Remote monitoring and support are also available from the VLLRO engineering team.
Q: Can the system operate in extreme cold weather?
A: Yes, as demonstrated by the Qinghai-Xizang Plateau project, the system can be customized with heating and insulation to operate reliably in sub-zero temperatures.
Q: What certifications does the equipment hold?
A: The equipment holds CE and ISO 9001 certifications, confirming compliance with international quality and safety standards.
Conclusion
The Containerized RO Plant from VLLRO offers a practical, rapidly deployable solution for water purification in remote areas, emergency situations, and challenging environments. Its factory-pre-installed design, customizable pretreatment options, and robust construction make it a reliable choice for communities, industries, and humanitarian organizations seeking clean water without the delays and costs of traditional plant construction. Backed by over 15 years of experience, CE and ISO 9001 certifications, and a commitment to quality, VLLRO provides a solution that meets the needs of diverse users. For inquiries, technical specifications, or to discuss your specific requirements, the VLLRO team is available to provide detailed product information and professional support.
Related News
- How to Reduce Wastewater in Commercial RO Systems Without Sacrificing Membrane Life
- How to Calculate ROI for a Commercial Water Refilling Station
- How to Design a Borehole Water Pretreatment System for Remote Commercial RO Stations
- The "Brain" Behind the System: How VLLRO's Intelligent IoT Control Platform Revolutionizes Water Management
- The Invisible Shield: Why UV Sterilization is Non-Negotiable for Safe Drinking Water
- Maximizing RO Longevity: The Complete Guide to Water Filtration Consumables and Replacement Cycles
Leave me a message