English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

How Does an Industrial Reverse Osmosis Water Purifier Deliver Reliable High‑Purity Water for Manufacturing and Processing?
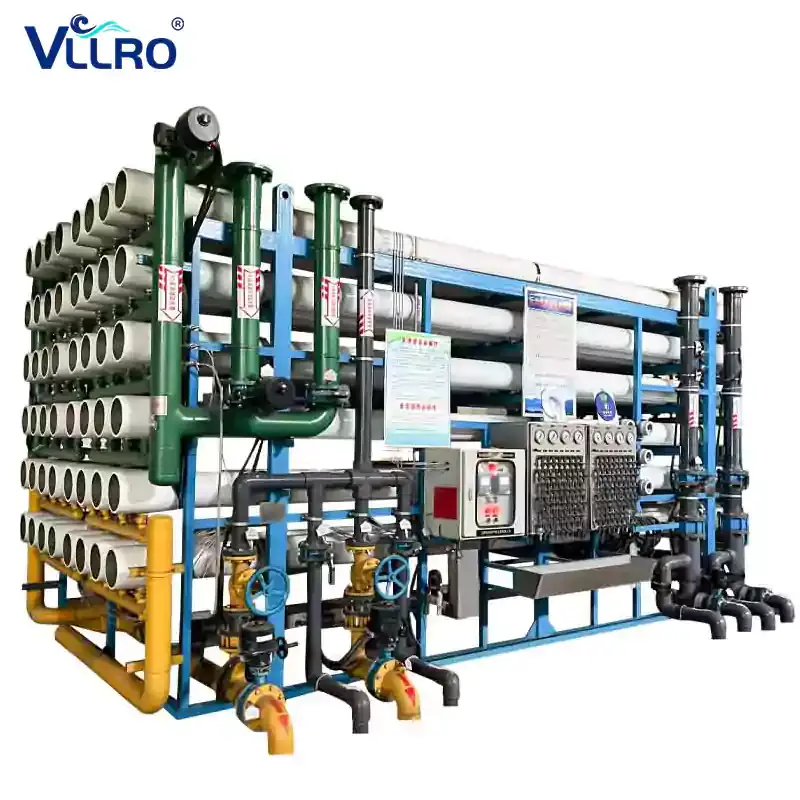
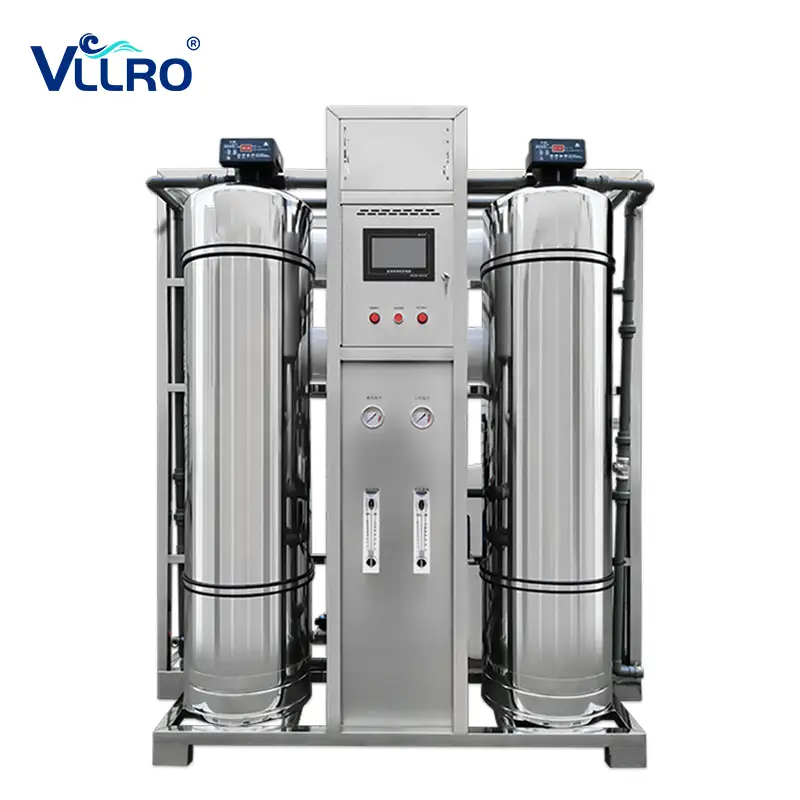
Industrial production often demands large volumes of consistent, high‑purity water for cleaning, processing, or product formulation. The Industrial Reverse Osmosis Water Purifier from VLLRO offers a robust, customisable solution that combines multi‑stage pre‑treatment, high‑efficiency RO membranes, and intelligent controls to produce up to 100 tons of pure water per hour. With a desalination rate of 99.4‑99.6%, this equipment supports applications ranging from food and beverage processing to electronics manufacturing. This article examines its technical configuration, key advantages, and the manufacturing expertise behind the VLLRO brand.
Why Industrial Processes Rely on Reverse Osmosis for Water Quality?
In many industries, tap water or raw well water is unsuitable for direct use due to dissolved solids, organic matter, or bacterial contamination. Poor water quality can lead to product defects, equipment scaling, and inconsistent results. Reverse osmosis (RO) has become the standard technology for industrial water purification because it effectively removes up to 99.6% of dissolved salts, bacteria, and organic compounds, delivering water that meets stringent quality specifications.
VLLRO has designed its Industrial Reverse Osmosis Water Purifier to meet these requirements with flexibility and reliability. The system handles raw water with TDS up to 1500 ppm and turbidity below 5 FTU, and can be configured with single‑stage or two‑stage RO processes. Whether you need 1 ton or 100 tons per hour, VLLRO provides a customised solution that ensures stable, on‑specification water for your production line.
System Configuration and Filtration Process
The VLLRO industrial RO system is built around a well‑engineered treatment train that adapts to varying feed water conditions. A typical configuration includes:
• Multi‑media filter – Removes suspended solids, sand, and silt to protect downstream components.
• Activated carbon filter – Adsorbs chlorine, organic compounds, and odours that could damage RO membranes.
• Softening filter (optional) – Reduces hardness to prevent scaling on membrane surfaces.
• Scale inhibitor dosing (optional) – Minimises scale formation in high‑hardness water.
• Precision filter – Provides final particulate removal before the RO stage.
• Reverse osmosis membrane stage – The core purification step, using HuiTong 8040 membranes (or equivalent) to achieve high salt rejection.
This layered approach ensures that the RO membranes operate under optimal conditions, extending their lifespan and reducing maintenance frequency.
Key Technical Specifications
The table below summarises the typical parameters for the Industrial Reverse Osmosis Water Purifier model VLLRO‑RO‑2.0 from VLLRO. Other capacities are available upon request.
| Parameter | Specification |
| Model | VLLRO‑RO‑2.0 |
| Process Flow | Sand → Carbon → Scale inhibitor (optional) → Precision filter → RO membrane |
| Dimensions (L×W×H) | 170 cm × 85 cm × 190 cm |
| Water Production | 2.0 tons per hour (customisable from 1 to 100 T/H) |
| Desalination Rate | 99.4% – 99.6% |
| Voltage | 110V / 220V / 380V (selectable) |
| Inlet Pressure | 0.2 – 0.4 MPa |
| RO Operating Pressure | 0.8 – 1.2 MPa |
| RO Membrane | HuiTong 8040 × 2 (or equivalent brand) |
| High‑Pressure Pump | SHIMGE (or equivalent international brand) |
| Filter Tank | 400 × 1650 mm |
| Precision Filter | PP cotton × 5 |
| Filter Media Volume | Sand: 180 kg; Carbon: 65 kg (with 40 kg sand underbed) |
| Inlet / Waste Outlet | DN25 |
| Pure Water Outlet | DN25 |
| Raw Water TDS Limit | <1500 ppm |
| Raw Water Temperature | 25°C (nominal) |
| Raw Water Turbidity | <5 FTU |
| Raw Water Iron Ion | <0.3 mg/L |
Intelligent Control and User Convenience
Modern industrial water treatment equipment must be easy to operate and maintain. VLLRO equips its purifiers with an intelligent control system that offers:
• One‑click start/stop – Simplifies daily operation for plant personnel.
• Online water quality monitoring – Continuous display of conductivity, flow, and pressure for real‑time process visibility.
• Automatic flushing – Regularly cleans the RO membranes to prevent fouling and maintain performance.
• Fault early warning – Alerts operators to potential issues before they cause downtime, enabling proactive maintenance.
These features reduce the need for constant human supervision, allowing the system to run reliably around the clock. The prefabricated skid‑mounted design also means that the unit is fully tested and debugged at the factory, so on‑site installation is quick and straightforward.
Applications Across Diverse Industries
The Industrial Reverse Osmosis Water Purifier is suitable for a wide range of sectors that require large volumes of purified water:
• Food and beverage processing – Ingredient water, cleaning, and steam generation.
• Electronics and semiconductor manufacturing – Ultra‑pure water for wafer rinsing and cleaning.
• Pharmaceutical and cosmetics – Water for formulation, blending, and final rinsing.
• Power generation – Boiler feedwater and cooling tower makeup.
• Schools, hospitals, and community water stations – Centralised drinking water supply.
• Hotels and resorts – Large‑scale water purification for guest rooms, kitchens, and laundry.
With customisable flow rates from 1 to 100 tons per hour, the system can be scaled to match the specific needs of each application.
Quality Components for Long‑Term Reliability
VLLRO selects only high‑quality components for its industrial RO systems to ensure durability and consistent performance. The high‑pressure pump is supplied by SHIMGE (or equivalent internationally recognised brands), and the RO membranes are sourced from HuiTong or comparable quality suppliers. Solenoid valves, sensors, and piping are chosen for corrosion resistance and long service life.
The system’s structure is fabricated using advanced equipment including laser cutting, robotic welding, and CNC bending, ensuring precise fit and finish. Every unit undergoes a rigorous 72‑hour pressure and performance test before dispatch, simulating real operating conditions to verify sealing, flow rates, and desalination efficiency. This commitment to quality is backed by ISO9001, ISO14001, and ISO45001 certifications.
Global Presence and Customer Support
VLLRO has served over 1,000 customers in more than 50 countries, providing water treatment solutions for industrial, commercial, and municipal applications. The company offers comprehensive pre‑ and post‑sales support, including water analysis, system design, installation guidance, and ongoing technical assistance. Spare parts are readily available, and the team provides remote troubleshooting to minimise downtime.
One recent project involved a well‑known semiconductor factory in Southeast Asia, where VLLRO supplied a 5 T/H reverse osmosis system for product cleaning and processing. The system operates 24 hours a day, delivering stable pure water quality and contributing to the customer's production efficiency. This case reflects VLLRO's capability to handle demanding industrial applications with tailored solutions and responsive service.
Frequently Asked Questions
Q: What is the maximum water production capacity of this industrial RO system?
A: The system can be customised to produce from 1 to 100 tons per hour, depending on the model and configuration. The standard model listed produces 2 T/H.
Q: What is the expected desalination rate?
A: The desalination rate is typically between 99.4% and 99.6%, ensuring high‑purity water suitable for most industrial applications.
Q: Can the system handle raw water with high turbidity or TDS?
A: Yes, the pre‑treatment section (multi‑media filter, carbon filter, and optional softener) is designed to handle turbidity below 5 FTU and TDS up to 1500 ppm. For higher TDS, additional pre‑treatment or a two‑stage RO design is available.
Q: Is the system easy to install and operate?
A: Absolutely. The unit is factory‑assembled and tested, requiring only connection to water, power, and drain lines. The intelligent control panel makes operation straightforward with minimal training.
Q: What after‑sales support does VLLRO provide?
A: We offer installation guidance, online technical support, spare parts supply, and a warranty period. Our engineering team is available for remote troubleshooting and on‑site visits if needed.
Q: Can I customise the system for my specific water quality and flow requirements?
A: Yes, VLLRO specialises in OEM/ODM solutions. We design each system based on your feed water analysis, required output quality, and space constraints.
Conclusion
The Industrial Reverse Osmosis Water Purifier from VLLRO delivers a reliable, efficient, and customisable solution for high‑purity water needs across multiple industries. With robust pre‑treatment, intelligent controls, and high‑quality components, it ensures stable operation and consistent water quality, even under demanding conditions. Backed by over 15 years of manufacturing experience, global export expertise, and a commitment to customer service, VLLRO is well‑positioned to support your water treatment requirements. Contact us today to discuss your project!
Related News
- How to Reduce Wastewater in Commercial RO Systems Without Sacrificing Membrane Life
- How to Calculate ROI for a Commercial Water Refilling Station
- How to Design a Borehole Water Pretreatment System for Remote Commercial RO Stations
- The "Brain" Behind the System: How VLLRO's Intelligent IoT Control Platform Revolutionizes Water Management
- The Invisible Shield: Why UV Sterilization is Non-Negotiable for Safe Drinking Water
- Maximizing RO Longevity: The Complete Guide to Water Filtration Consumables and Replacement Cycles
Leave me a message