English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

Why Is the Reverse Osmosis Water System the Ideal Solution for High-Purity Water Needs?
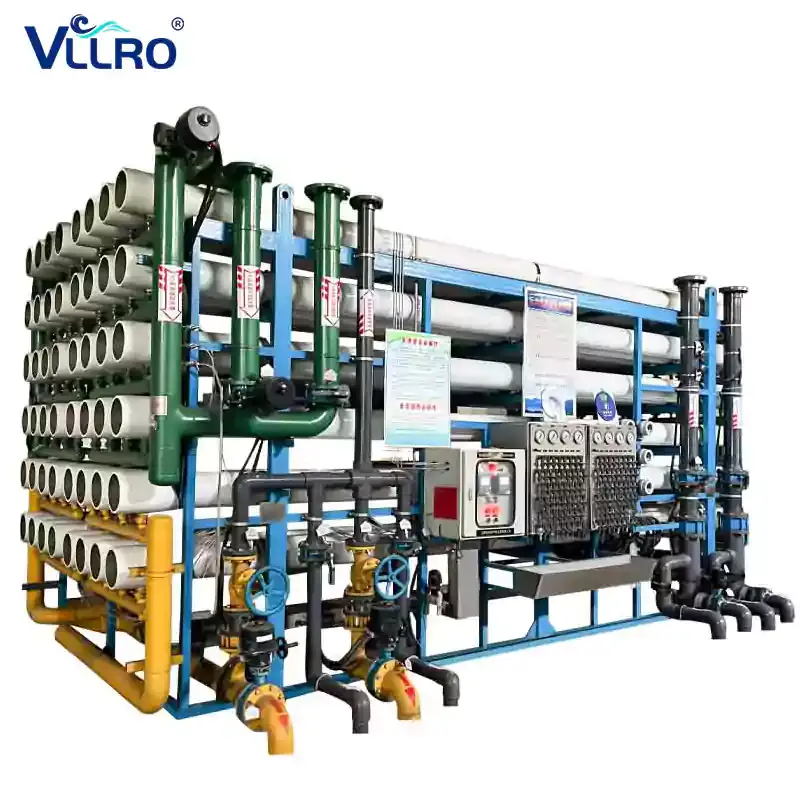
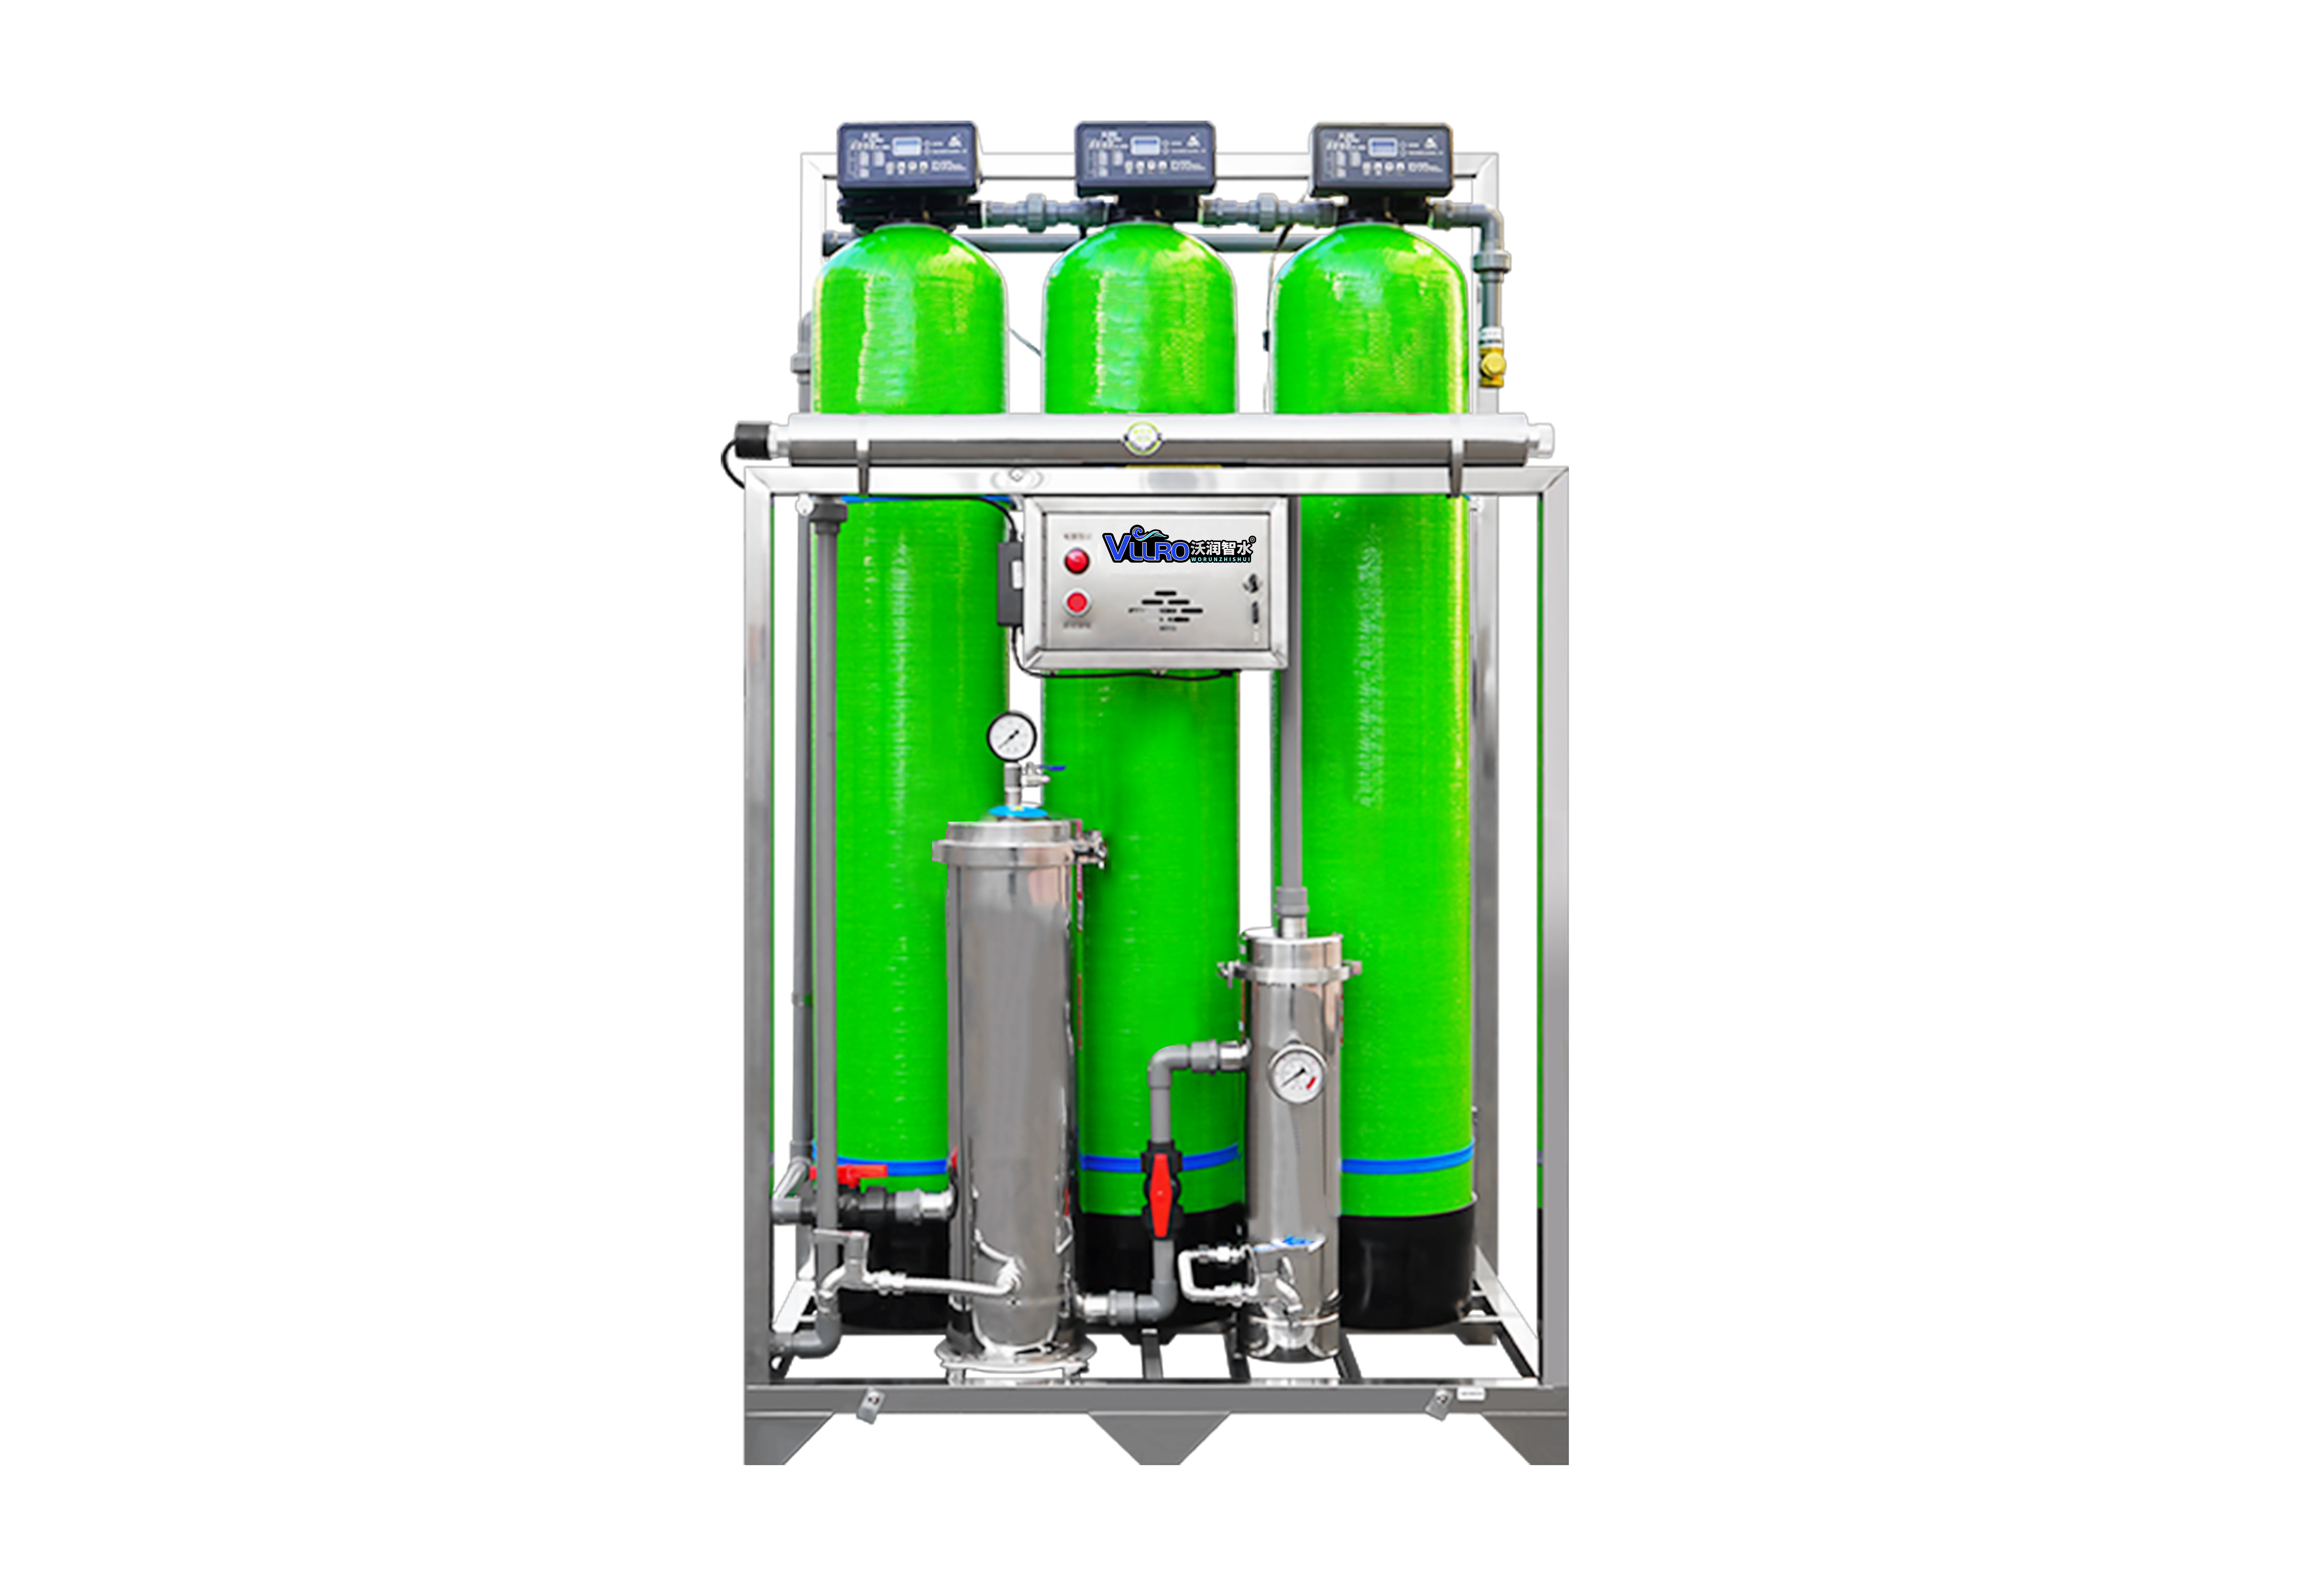
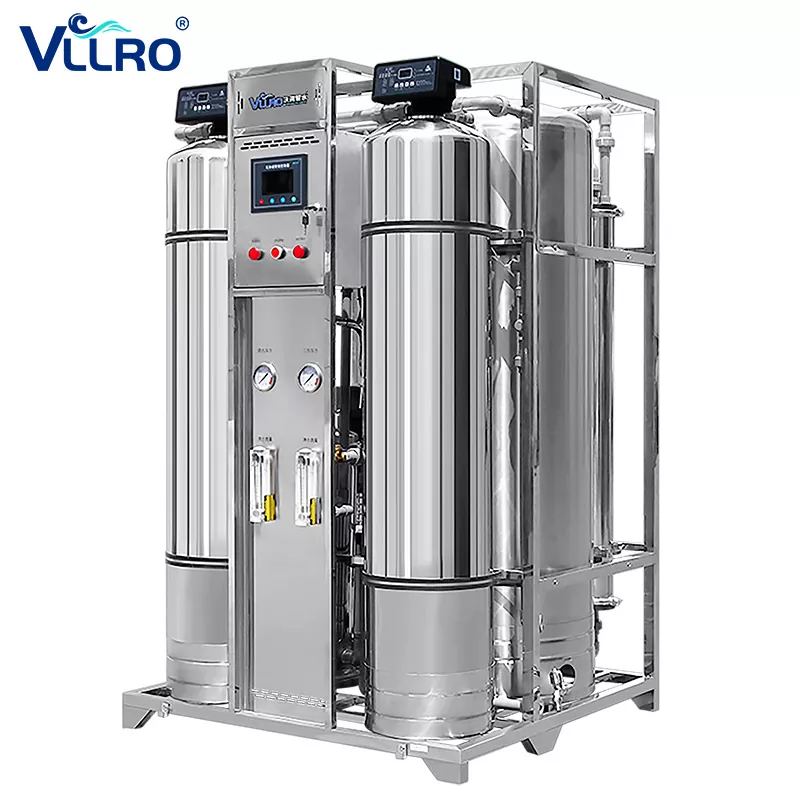
Access to high-quality purified water is essential across a wide range of applications—from drinking water and food processing to electronics manufacturing and commercial facilities. The Reverse Osmosis Water System from VLLRO offers a reliable, efficient solution for producing pure water with a high desalination rate of 99.40%. Featuring a multi-stage pre-treatment system, advanced RO membranes, and an intelligent control system, this equipment delivers stable water production while minimizing waste and energy consumption. This article examines the product's specifications, key features, and the applications where it delivers significant value for both residential and commercial users.
The Need for Reliable Water Purification
Water quality is a critical concern across industries and communities. Whether for drinking, food processing, electronics manufacturing, or commercial use, the demand for consistently pure water continues to grow. Standard tap water often contains dissolved solids, bacteria, and other impurities that can affect product quality, equipment performance, and human health. The Reverse Osmosis Water System from VLLRO addresses these challenges by using advanced RO membrane technology to remove up to 99.4% of dissolved impurities, producing water that meets the highest purity standards.
The system is designed for both civilian and commercial applications, offering a versatile solution that can be customized to meet specific water quality and production requirements. With a water yield of 1.0 tons per hour and support for various voltage configurations (110V/220V/380V), it is suitable for a wide range of scenarios—from small-scale commercial operations to large-scale industrial processes. The equipment's modular design and intelligent control system ensure ease of operation, automatic flushing, water shortage protection, and fault alarm functions, making it a practical choice for users with varying levels of technical expertise.
Technical Specifications
The following table summarizes the key specifications for the Reverse Osmosis Water System (Model VLLRO-RO-1.0) from VLLRO.
| Parameter | Specification Details |
| Model | VLLRO-RO-1.0 |
| Process Flow | Sand → Carbon → Scale Inhibitor (optional) → Precision Filter → RO Membrane |
| Dimensions | 101 cm × 100 cm × 162 cm |
| Desalination Rate | 99.40% |
| Water Yield | 1.0 T/H |
| Voltage | 110V / 220V / 380V (selectable) |
| Inlet Pressure | 0.2 – 0.4 MPa |
| RO Pressure | 0.8 – 1.2 MPa |
| RO Membrane | HuiTong 4040 × 4 |
| High Pressure Pump | SHIMGE |
| Filter Tank | 300 × 1400 mm |
| Precision Filter | PP cotton × 5 |
| Filter Tank Filling | Sand (80 kg) + Carbon (13 kg sand + 28 kg carbon) |
| Water Tank Volume | 300 L |
| Water Tank Material | 304 Stainless Steel |
| Water Inlet / Waste Outlet | 6' (3/4 in) |
| Pure Water Outlet | 4' (1/2 in) |
| Raw Water TDS | < 1500 ppm |
| Raw Water Temperature | 25°C |
| Raw Water Turbidity | < 5 FTU |
| Raw Water Iron Ion | < 0.3 mg/L |
These specifications reflect the system's capability to produce high-purity water consistently, with robust pre-treatment and filtration stages that protect the RO membranes and extend their service life.
Key Features and Performance Advantages
The system incorporates several design features that enhance its performance, durability, and ease of use.
Advanced RO Membrane Technology
The system uses industry-leading RO membranes that deliver a high desalination rate of 99.40%, effectively removing dissolved solids, bacteria, and other impurities. This ensures that the water produced meets high-purity standards for drinking, food processing, and industrial applications. The membranes are selected for their long service life and stable performance, reducing the frequency of replacements and lowering long-term operating costs.
Intelligent Control System
The equipment features an intelligent control system that simplifies operation and monitoring. Functions include automatic flushing to keep the membranes clean, water shortage protection to prevent pump damage, and fault alarms to alert operators to issues. The control interface can be customized according to customer needs, making the system adaptable to different operational requirements and user preferences.
Durable Stainless Steel Construction
The equipment frame is constructed from stainless steel, providing excellent corrosion resistance and a long service life. The modular layout ensures efficient use of space and provides ample access for maintenance of components such as the filter tanks, pump, and membrane housings. This design simplifies the replacement of filter media and routine maintenance, reducing downtime and service costs.
Water and Energy Efficiency
The system is designed to minimize wastewater discharge and reduce energy consumption. The energy-saving technology helps lower electricity costs, while the reduced waste output makes the system more environmentally friendly. All components are standardized and available worldwide, ensuring simple and fast maintenance.
Applications Across Industries
The Reverse Osmosis Water System is suitable for a wide range of applications across various industries:
• Food and beverage industry – Used for raw material cleaning, formula water preparation, and beverage preparation, ensuring product taste and safety.
• Electronics and semiconductor industry – Provides ultra-pure water pretreatment for cleaning circuit boards and semiconductor components.
• Hotels and commercial centers – Supplies high-quality water for central kitchens, swimming pools, and SPA clubs.
• Educational institutions – Provides clean drinking water for schools and universities, as demonstrated in a project serving over 200 primary and secondary schools in Malaysia.
• Healthcare facilities – Supplies purified water for medical equipment, laboratory use, and patient hydration.
• Industrial manufacturing – Used in processes requiring high-purity water, such as boiler feed water and product rinsing.
The system's versatility and reliable performance make it a practical choice for these diverse applications.
Quality Assurance and Manufacturing Capabilities
VLLRO is backed by Jianyun Zhishui (Qingdao) Industrial Technology Co., Ltd., a water treatment equipment manufacturer with over 15 years of industry experience. The company operates two modern production bases totaling more than 12,000 square meters, equipped with advanced facilities including laser cutting machines, welding robots, and automated assembly lines.
Each system undergoes a rigorous 72-hour test before leaving the factory, including pressure tests, performance tests, and debugging of automated programs. This ensures that the equipment meets the required standards for quality and reliability. The company holds CE and ISO 9001 certifications and can assist customers in meeting specific market certifications such as NSF and FDA. Professional OEM/ODM services are available, allowing customers to customize products and solutions based on site conditions, water quality, and production requirements.
Frequently Asked Questions
Q: What is the desalination rate of this system?
A: The system achieves a desalination rate of 99.40%, effectively removing dissolved solids and impurities from the water.
Q: Can the system be customized?
A: Yes. VLLRO offers professional OEM/ODM services and can customize products and solutions based on your site conditions, water quality, and production requirements.
Q: What is the typical water yield of this system?
A: The standard model (VLLRO-RO-1.0) has a water yield of 1.0 tons per hour. Other capacities are available upon request.
Q: Does the system require regular maintenance?
A: Yes, regular maintenance of filter media and membrane elements is recommended to ensure optimal performance and service life. The modular design and standardized components make maintenance straightforward and cost-effective.
Q: What certifications does the product hold?
A: The products and core components have obtained CE and ISO 9001 certifications. Assistance with meeting specific market certifications such as NSF and FDA is also available.
Q: How long does the equipment undergo testing before shipment?
A: Each system undergoes a rigorous 72-hour test before leaving the factory, including pressure tests, performance tests, and debugging of automated programs.
Conclusion
The Reverse Osmosis Water System from VLLRO offers a reliable, efficient solution for producing high-purity water across a wide range of applications. With its advanced RO membrane technology, intelligent control system, and durable stainless steel construction, it delivers consistent performance and long-term value. Backed by over 15 years of industry experience, CE and ISO 9001 certifications, and a commitment to quality, VLLRO provides water treatment systems that meet the needs of food processing, electronics, commercial, and institutional users. For inquiries, technical specifications, or to discuss your specific requirements, the VLLRO team is available to provide detailed product information and professional support.
Related News
- How to Reduce Wastewater in Commercial RO Systems Without Sacrificing Membrane Life
- How to Calculate ROI for a Commercial Water Refilling Station
- How to Design a Borehole Water Pretreatment System for Remote Commercial RO Stations
- The "Brain" Behind the System: How VLLRO's Intelligent IoT Control Platform Revolutionizes Water Management
- The Invisible Shield: Why UV Sterilization is Non-Negotiable for Safe Drinking Water
- Maximizing RO Longevity: The Complete Guide to Water Filtration Consumables and Replacement Cycles
Leave me a message