English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик

Why Is Customized Water Treatment Equipment the Key to Solving Complex Water Quality Challenges?
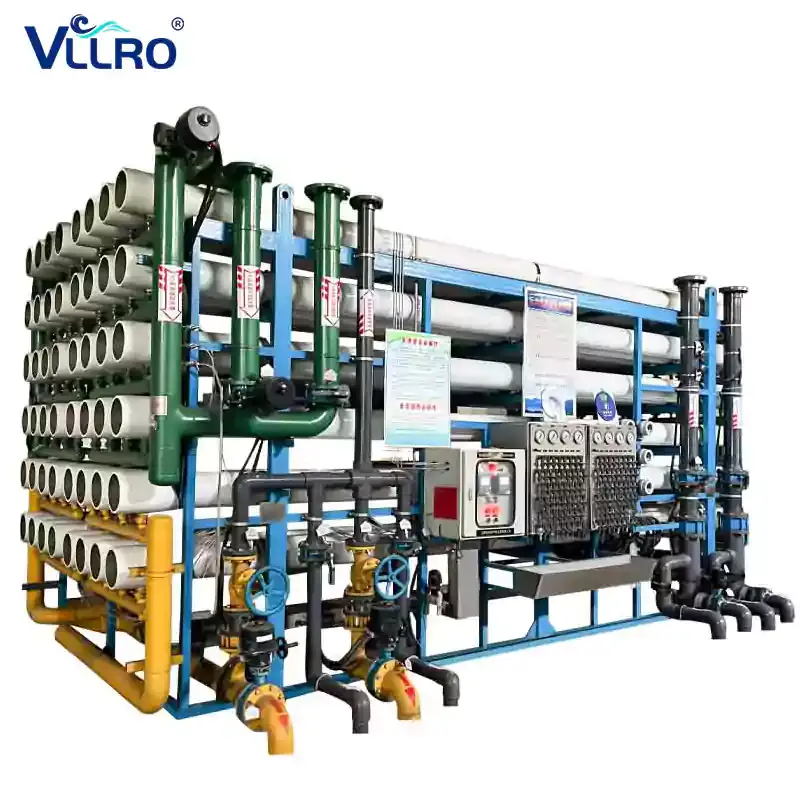
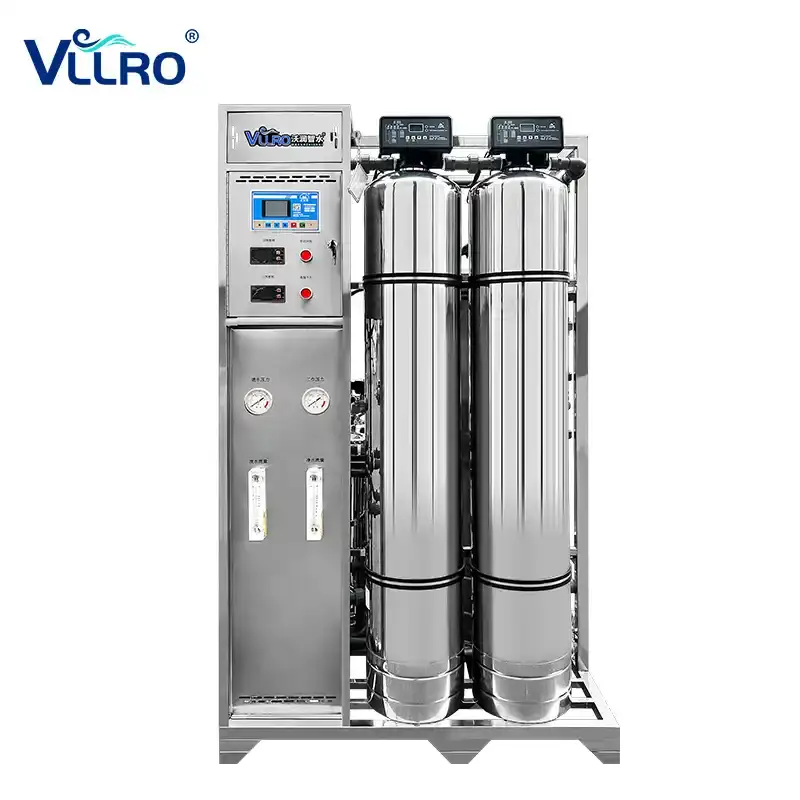
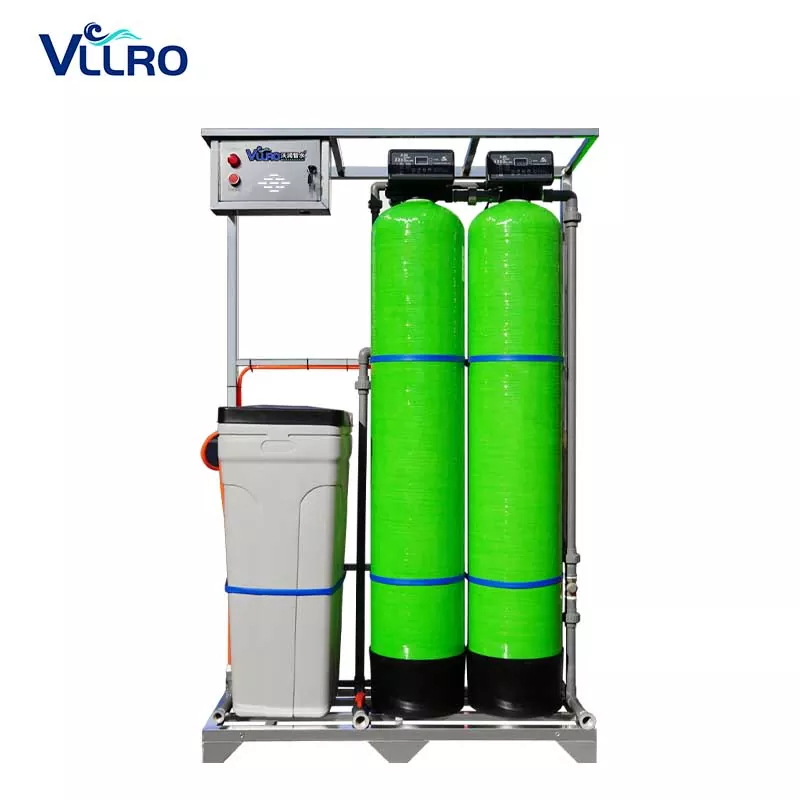
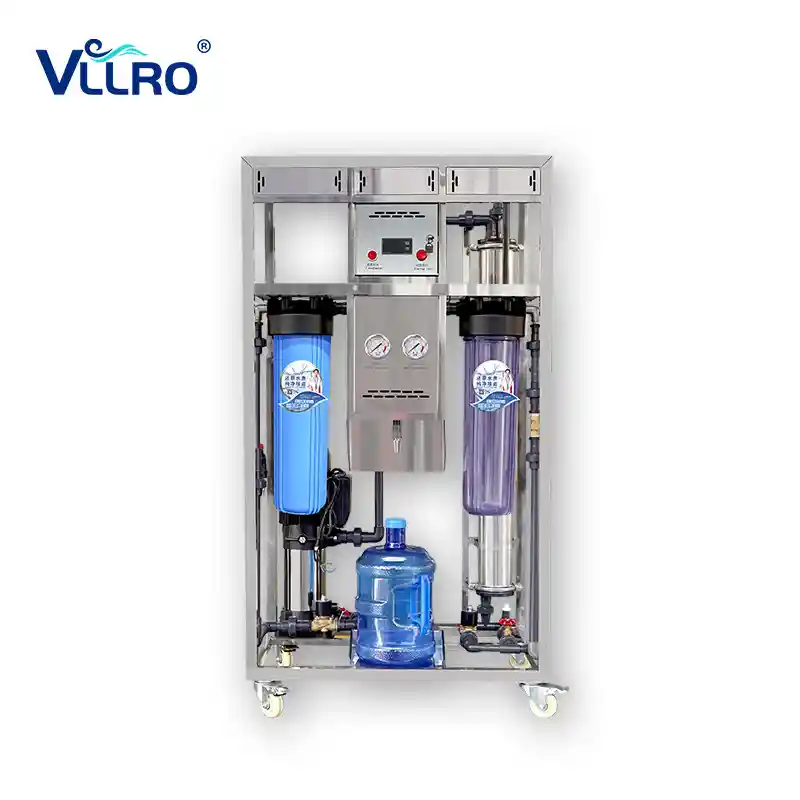
Standard water treatment equipment often falls short when faced with varying raw water quality, unique installation constraints, and specific usage requirements. Off-the-shelf solutions may include unnecessary functions or fail to address critical issues, leading to wasted investment and ongoing operational problems. The Water Treatment Equipment from VLLRO offers a practical alternative: deep customization based on raw water quality reports, water consumption data, and on-site conditions. With over 15 years of industry experience, an in-house engineering team, and a modern manufacturing facility in Qingdao, VLLRO designs and produces systems that match specific application needs. This article examines the product's features, technical specifications, and the real-world case studies that demonstrate its value.

Why Standard Equipment Often Misses the Mark?
Many water treatment projects face a common problem: the equipment available on the market is designed for average conditions, but actual water quality varies significantly. Raw water TDS levels, turbidity, iron content, and temperature fluctuate across regions and seasons. Installation spaces differ from one site to another. Usage patterns—whether for community drinking water, industrial processing, or commercial applications—require different configurations. When standard equipment is installed without proper adaptation, the result is often inefficient operation, frequent breakdowns, and higher long-term costs.
The Water Treatment Equipment from VLLRO addresses this issue through a deep customization approach. Rather than forcing a standard design into a unique situation, the engineering team begins with a thorough analysis of the raw water quality report (TDS, hardness, turbidity, iron content), water consumption requirements, and the physical installation space. This data-driven approach ensures that every component—from pumps and membrane elements to valves and controllers—is selected to match the actual operating conditions. The result is equipment that performs reliably, with no wasted functions or unnecessary costs.
Technical Specifications
The following table summarizes the key specifications for a typical Water Treatment Equipment model (VLLRO-RO-3.0) from VLLRO.
| Parameter | Specification Details |
| Model | VLLRO-RO-3.0 |
| Process Flow | Sand → Carbon → Scale Inhibitor (optional) → Precision Filter → RO Membrane |
| Dimensions | 190 cm × 120 cm × 220 cm |
| Desalination Rate | 99.40% |
| Water Yield | 3.0 T/H |
| Voltage | 110V / 220V / 380V (selectable) |
| Inlet Pressure | 0.2 – 0.4 MPa |
| RO Pressure | 0.8 – 1.2 MPa |
| RO Membrane | HuiTong 8040 × 3 |
| High Pressure Pump | SHIMGE |
| Filter Tank | 600 × 1900 mm |
| Precision Filter | PP cotton × 5 |
| Filter Tank Filling | Sand (500 kg) + Carbon (80 kg sand + 125 kg carbon) |
| Water Inlet / Waste Outlet | DN40 (1 1/2") |
| Pure Water Outlet | DN25 (1") |
| Raw Water TDS | < 1500 ppm |
| Raw Water Temperature | 25°C |
| Raw Water Turbidity | < 5 FTU |
| Raw Water Iron Ion | < 0.3 mg/L |
These specifications represent a standard configuration, but each system is customized based on the specific water quality and operational requirements of the project. The modular design allows for adjustments to meet different capacity needs, from small community systems to large industrial installations.
The Customization Process: From Water Analysis to Delivery
The development of a customized water treatment system follows a structured process that ensures the final product meets the specific needs of each application.
Step 1: Demand Analysis
The process begins with a thorough analysis of the source water quality, water usage requirements, pressure needs, and installation space constraints. Customers provide raw water quality data (TDS, hardness, turbidity, iron content) or water samples for testing. This information forms the basis for all subsequent design decisions.
Step 2: Solution and Design Customization
Based on the demand analysis, the engineering team designs a customized solution tailored to the application scenario—whether industrial water, commercial drinking water, or household water purification. The design includes equipment sizing, processing capacity, brand logo placement, exterior color, and control system configuration.
Step 3: Product and Accessory Customization
Core components such as pumps, membrane elements, and valves are selected to balance performance and budget. The equipment is manufactured to meet the specific requirements of the project, with non-standard designs accommodated as needed.
Step 4: Testing and Delivery
Each customized system undergoes rigorous factory testing, including stress testing and performance verification, before shipment. This ensures that the equipment meets the required standards before being delivered to customers worldwide.
This structured approach ensures that every system is optimized for its intended application, with no wasted capacity or unnecessary features.
Real-World Application: Community Water Treatment in Southeast Asia
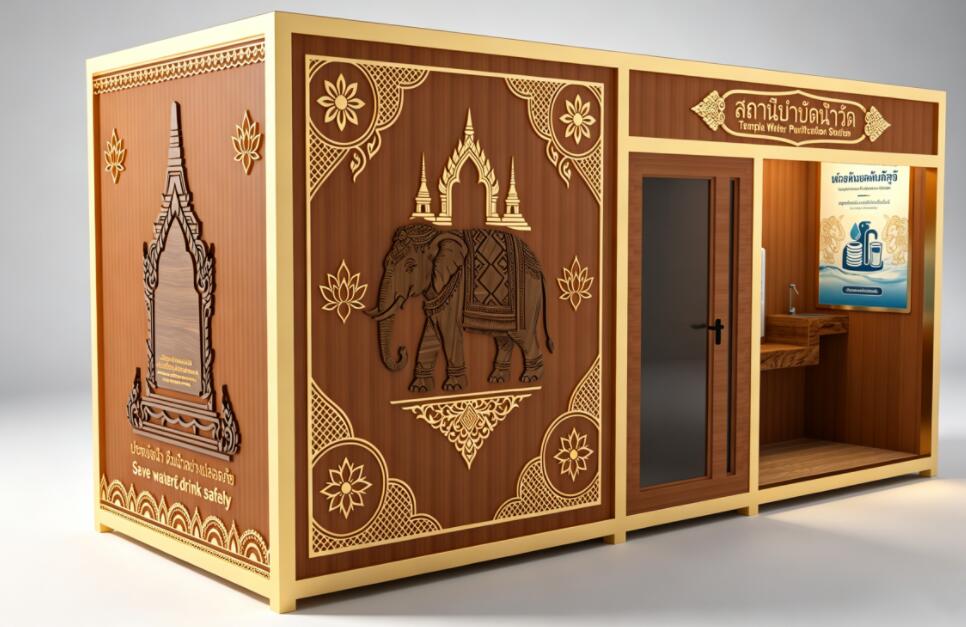
A case study from Southeast Asia illustrates the value of customized water treatment equipment. A client needed to supply clean drinking water to multiple communities, each with different water quality issues and installation constraints. The water pollution problems varied from one community to another, and the installation locations and available spaces were all different. Standard equipment was not suitable because each system required unique specifications, making production costs prohibitively high with most manufacturers.
VLLRO took on the project because of its in-house manufacturing capabilities. With a complete production line covering sheet metal processing, welding, circuitry, and final assembly and commissioning, the company was able to minimize costs while delivering fully customized systems. The equipment was produced, inspected, and delivered within the customer's requirements, meeting the diverse needs of each community and receiving recognition and satisfaction from the client.
This case demonstrates the advantage of working with a manufacturer that controls the entire production process. By integrating engineering design, manufacturing, and quality control under one roof, VLLRO can respond flexibly to unique requirements while maintaining cost-effectiveness.
Quality Assurance and Manufacturing Capabilities
VLLRO is backed by Jianyun Zhishui (Qingdao) Industrial Technology Co., Ltd., a water treatment equipment manufacturer with over 15 years of industry experience. The company operates two modern production bases totaling more than 12,000 square meters, with highly automated production lines and a rigorous quality control system.
Key manufacturing capabilities include:
• Automatic laser cutting machines and laser pipe cutting machines for millimeter-level precision in steel plate and tube cutting.
• Fully automatic welding robots for unmanned and standardized welding of key components, ensuring structural strength and leak-tightness.
• CNC press brakes, shearing machines, and round rolling machines for efficient sheet metal processing.
• Laser marking machines for permanent brand logos, model numbers, and production information on each equipment and core component.
The company's quality control system includes a 100% batch inspection for raw materials and a rigorous 72-hour extreme pressure simulation test for every unit before shipment. This testing verifies sealing, structural integrity, and operational stability under various conditions, ensuring that the equipment arrives ready for reliable service.
Frequently Asked Questions
Q: Can you provide a large-scale solution for community or factory water supply?
A: Yes. We not only provide household and commercial equipment but also specialize in large-scale industrial and municipal water treatment projects. We have rich experience in designing, manufacturing, and installing large-scale reverse osmosis systems, multi-media filtration systems, and fully automatic constant pressure water supply systems. We can customize non-standard solutions based on your specific needs and water volume.
Q: Do you support OEM/ODM customization?
A: Yes. We support both OEM and ODM cooperation. Customizations include product appearance, product performance, system configuration, treatment capacity, core component selection based on target market water quality, brand identity, and packaging. We also assist with certification requirements in different countries.
Q: Is the equipment complicated to install and operate?
A: No. We provide detailed installation manuals, video tutorials, and online remote guidance. Most of our equipment is fully automatic and only requires regular maintenance. We also provide lifetime technical support and guarantee a long-term supply of all wearing parts and spare parts (such as filter elements, membrane elements, and sealing rings).
Q: How do overseas traders or distributors purchase your products?
A: We welcome cooperation with distributors worldwide. The process typically involves: contacting us with your target market and needs; receiving recommended products and competitive quotes; determining product configuration, logo customization, packaging, and payment method; signing a formal purchase contract; and receiving delivery to your designated port by sea, air, or other logistics options.
Q: What payment methods and delivery cycles are available?
A: We support various secure international payment methods to suit different customer needs. For standard products, we have a large inventory and can ship on the same day. For customized products, the production cycle is based on configuration and quantity, and our sales manager will provide an accurate delivery date.
Q: What is the warranty period for water treatment equipment?
A: We provide a clear quality warranty period for all products—typically 1 year for the whole machine, with longer warranties for core components such as membrane shells and pumps. During the warranty period, we provide free repair or component replacement for failures caused by product quality issues.
Conclusion
The Water Treatment Equipment from VLLRO offers a practical solution for organizations facing diverse water quality challenges. Through deep customization based on raw water analysis, consumption requirements, and installation constraints, each system is designed to match specific application needs without wasted capacity. With over 15 years of experience, in-house manufacturing, and a comprehensive quality assurance program, VLLRO provides reliable equipment for community water supply, industrial processing, and commercial applications. For inquiries, technical specifications, or to discuss your water treatment requirements, the VLLRO team is available to provide detailed product information and professional support.
Related News
- What Are the Main Stages of an Industrial Water Purification Process?
- How to Reduce Wastewater in Commercial RO Systems Without Sacrificing Membrane Life
- How to Calculate ROI for a Commercial Water Refilling Station
- How to Design a Borehole Water Pretreatment System for Remote Commercial RO Stations
- The "Brain" Behind the System: How VLLRO's Intelligent IoT Control Platform Revolutionizes Water Management
- The Invisible Shield: Why UV Sterilization is Non-Negotiable for Safe Drinking Water
Leave me a message